
Latest Products
Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com

2MK2102 Horizontal Deep Hole Honing Machine
1. Main Functions of the Machine Tool This machine tool is designed for finish machining of cylindrical deep-hole parts such as hydraulic cylinders and air cylinders. It supports both full-length honing and partial honing. For partial honing, it can correct taper, ovality and local aperture errors of workpieces. The expansion and contraction of the honing head is controlled by a servo motor, enabling both constant-pressure feed and fixed-quantity feed of the honing head. For constant-pressure feed: the total feed pressure remains constant. As surface roughness reduces continuously during honing, the contact points between the honing stones (also known as honing sticks) and the workpiece surface keep increasing. Consequently, the specific pressure exerted by the honing stones on the surface decreases gradually, which reduces the cutting action of the honing stones. When high spots are encountered during machining, the constant-pressure machining mode prevents sudden overload of the spindle motor. The controllable and evenly distributed pressure during machining delivers an excellent finished surface, with a maximum precision of Ra0.2. For fixed-quantity feed: the honing stones expand and feed forcibly at a preset speed. After the honing head enters the bore and expands rapidly to approach the workpiece surface, the honing stones are forced to expand further, generating a self-sharpening effect. This feed mode not only achieves low surface roughness but also corrects geometric errors of the bore. The hybrid feed mode combining constant-pressure feed and fixed-quantity feed effectively improves honing accuracy and efficiency. All castings of the machine tool are made of high-strength cast iron with resin sand molding. All castings undergo normalizing treatment after casting to eliminate internal stress generated during casting. After rough machining, a second normalizing treatment is carried out to further remove casting internal stress as well as the machining stress induced in roughing, so as to guarantee excellent precision stability.
Description
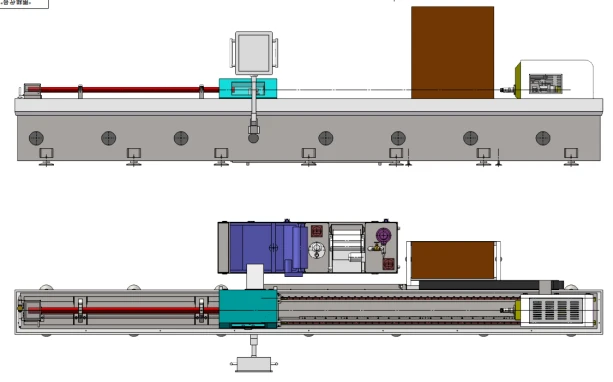
1.Main Functions of the Machine Tool
This machine tool is designed for finish machining of cylindrical deep-hole parts such as hydraulic cylinders and air cylinders. It supports both full-length honing and partial honing. For partial honing, it can correct taper, ovality and local aperture errors of workpieces.
The expansion and contraction of the honing head is controlled by a servo motor, enabling both constant-pressure feed and fixed-quantity feed of the honing head.
For constant-pressure feed: the total feed pressure remains constant. As surface roughness reduces continuously during honing, the contact points between the honing stones (also known as honing sticks) and the workpiece surface keep increasing. Consequently, the specific pressure exerted by the honing stones on the surface decreases gradually, which reduces the cutting action of the honing stones. When high spots are encountered during machining, the constant-pressure machining mode prevents sudden overload of the spindle motor. The controllable and evenly distributed pressure during machining delivers an excellent finished surface, with a maximum precision of Ra0.2.
For fixed-quantity feed: the honing stones expand and feed forcibly at a preset speed. After the honing head enters the bore and expands rapidly to approach the workpiece surface, the honing stones are forced to expand further, generating a self-sharpening effect. This feed mode not only achieves low surface roughness but also corrects geometric errors of the bore.
The hybrid feed mode combining constant-pressure feed and fixed-quantity feed effectively improves honing accuracy and efficiency.
All castings of the machine tool are made of high-strength cast iron with resin sand molding. All castings undergo normalizing treatment after casting to eliminate internal stress generated during casting. After rough machining, a second normalizing treatment is carried out to further remove casting internal stress as well as the machining stress induced in roughing, so as to guarantee excellent precision stability.
2.1 Bed
The machine bed adopts a split combined structure, assembled with high-strength bolts and positioned by taper pins.
Linear guideways are fitted on the bed for the spindle headstock. A rack is mounted on the inner side of the bed to drive the reciprocating movement of the headstock, meeting the requirement of high-speed travel for honing operations.
Two rectangular guideways on the bed support the workpiece. These guideways are quenched for superior wear resistance.
Guards are installed outside the guideways, featuring excellent leakage-proof performance.
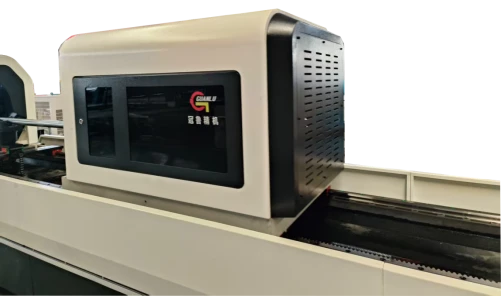
2.2 Headstock
The headstock is used to drive the rotation of the cutting tool and deliver high torque. Its transmission system consists of a motor, transmission mechanism and other components.
The headstock is equipped with a servo expansion system to control the expansion and contraction of the honing tool. The servo expansion system comprises a servo motor, precision planetary reducer, ball screw and other parts. The expansion and contraction of the honing head is controlled by the servo motor, which supports both constant-pressure feed and fixed-quantity feed of the honing head.
2.3 Workpiece Support Frame
The workpiece is placed on two sets of workpiece support frames and clamped tightly by pressure plates.
2.4 Honing Mandrel Support
The honing mandrel support shares the linear guideways with the headstock, and it is used to support the honing mandrel during machining.
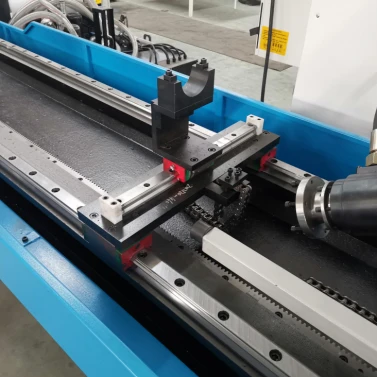
2.5 Honing Mandrel Bracket
The honing mandrel bracket is fixed on the machine bed to support the honing mandrel during machining and measurement.
2.6 Cooling System
The cooling system mainly uses circulating liquid medium to lubricate and cool the cutting zone, and remove chips at the same time.
2.7 Lubrication System
The guideway slides for reciprocating movement of the headstock are automatically lubricated by an automatic lubrication station which is equipped with liquid level alarm.
2.8 Control System
It adopts a separate electric cabinet with good dustproof performance. The cabinet is fitted with a cooling system to keep electrical components working under suitable temperature conditions, so as to extend the service life of components and ensure stable and reliable operation of the control system.
3.Main Technical Parameters of Machine Tool
Machining Range
Machining bore diameter range: Φ5~Φ20mm
Maximum machining depth: 1500mm
Workpiece outer diameter range: Φ25~Φ80mm
Workpiece length range: 250~1500mm
Machine Tool Performance
Z-axis (Headstock reciprocating motion) Reciprocating speed range: 1~40m/min
Servo motor rated power: 2.1kW
X-axis (Tool feed) Rapid traverse speed of push rod: 600mm/min
Maximum thrust force of push rod: 20kN
Servo motor rated power: 0.8kW
Headstock
Speed range: 10~600r/min, stepless speed regulation
Motor rated power: 1.5kW, servo motor
Others
Machine tool load capacity: 300kg
Total power of machine tool: approx. 6kW
Overall dimension of machine tool: 5.5m×2.5m×2.2m (Length × Width × Height)
Cooling System
Maximum flow rate: 60L/min
Motor power: 0.25kW
Tank capacity: approx. 900L
Filtration accuracy: 20μm
5.Contact Me
Email:sale@dzguanlu.com
Whatsapp/Wechat:+8613853423246
Hot Tags: 2mk2102 horizontal deep hole honing machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like


