Latest Products
Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com

BTA Deep Hole Drilling And Boring Machine
Deep hole drilling and boring machine Brief Machine processing capacity Drilling diameter range : Φ40~Φ100mm Boring diameter range : Φ40~Φ360mm Workpiece OD range: Φ90~Φ500mm Deep hole drilling and boring machine F unction: Drilling , Boring and Rolling . Drilling hole :...
Description
Deep hole drilling and boring machine Brief
Machine processing capacity
Drilling diameter range : Φ40~Φ100mm
Boring diameter range : Φ40~Φ360mm
Workpiece OD range: Φ90~Φ500mm
Deep hole drilling and boring machine Function:
Drilling , Boring and Rolling .
Drilling hole : BTA drilling method,remove the cutting chips backward through drill bar.
Boring hole: Adopt push boring method, remove the cutting chips forward through the
basic hole of workpiece.
Deep hole drilling and boring Machine main structure:
1.3.1 Machine main parts:
Machine bed , Headstock, Oil pressure head, Drill bar support rest, Drill box, Sliding guide rail,Rack and pinion,Coolant system,Siemens PLC control system,Electric cabinet,Center rest, Workpiece carrier and so on .
1.3.2 Workpiece clamping
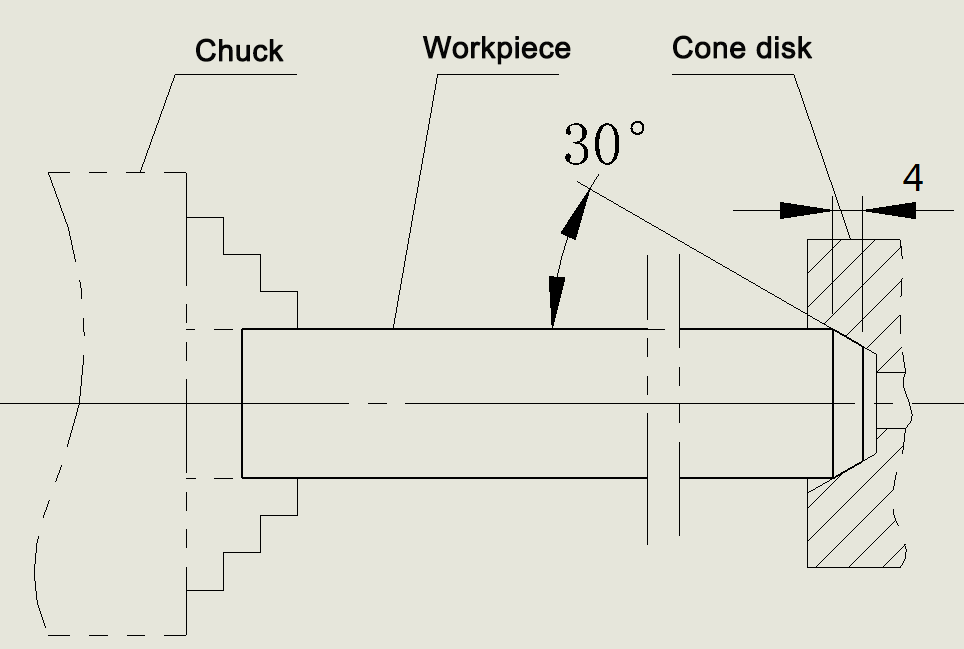
One end of the workpiece is clamped by the manual three-jaw chuck of headstock , oil pressure head tighten another end automatically(workpiece OD chamfer 4X30°), center rest support the workpiece .
1.3.3 Machine Control System :
Control system: PLC
Z1 axis: The longitudinal feed movement of the drilling box, the servo motor drives the rack and pinion mechanism through the reducing mechanism.
Z2 axis: Oil pressure head servo tighten the workpiecec, the servo motor drives the rack and pinion mechanism through the reducing mechanism.
1.3.4 The machine bed , box body, carriage etc. basic parts are precisely cast by super casting iron, processed by twice aging treatment after casting ,to eliminate stress , stable the structure and size , improve the mechanical properties ,etc. .
1.3.5 Machine bed
The machine bed is made of resin sand and normalised after casting. If the processing depth is more than one meter, machine bed adopts split structure, assembled with high strength bolts and positioned by cone pin.
Adopt double rectangular sliding guide rail, precision grinding, the guide rail surface is with high quenching hardness .
The width of guide rail is large ; The rack which is treated by precision processing and quenching is mounted inside of machine bed ,used for cutting tool feeding drive. The machine has large bearing capacity, good rigidity and stable transmission.
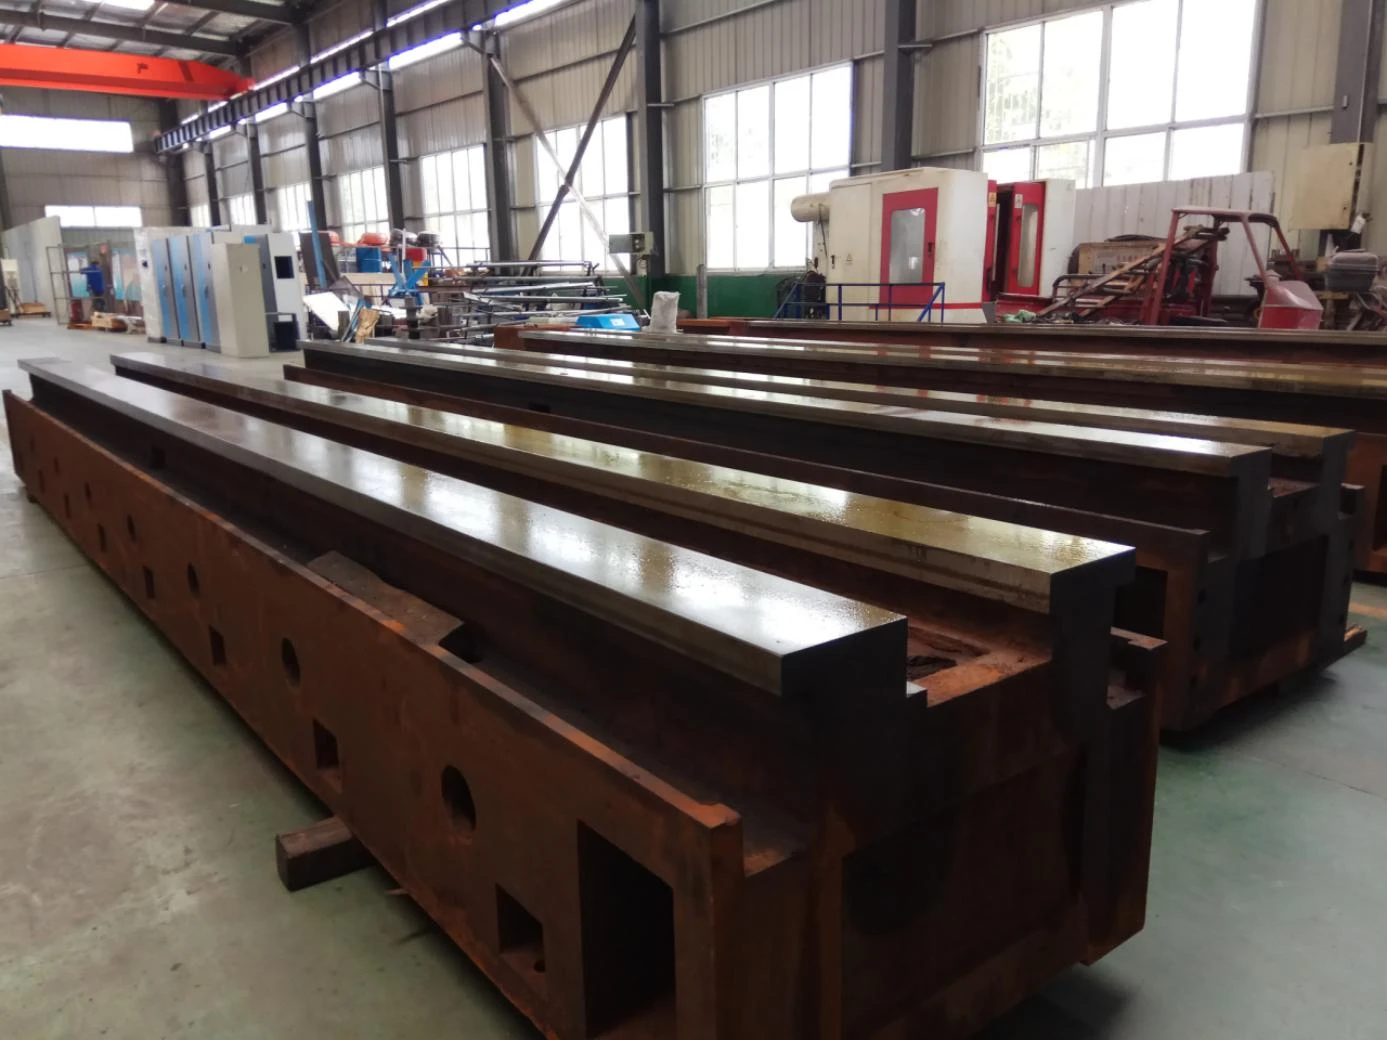
The V-shaped slant reinforcement are distributed inside of the machine bed , supporting strength is high, and it is not easy to deform; The outer wall of machine bed support the guide rail directly, so the guide rail could bear large cutting force, with good rigidity, not easy to deform and vibrate during machining, it is good for improving the processing quality and working efficiency of machine .
Apron type protection is assembled around the machine bed .
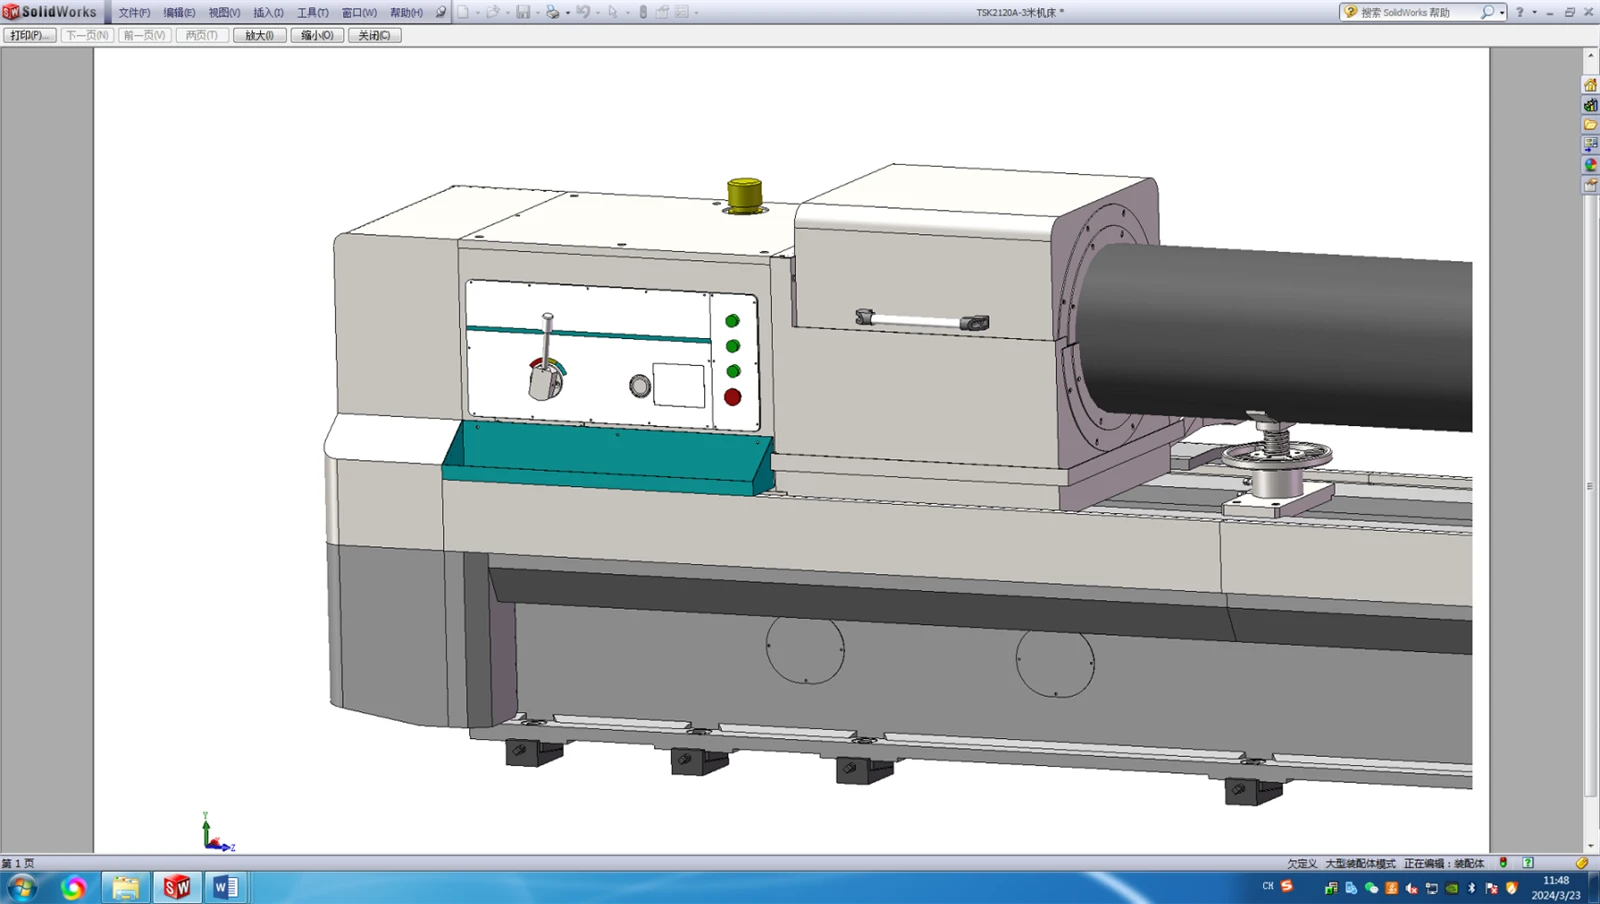
1.3.6 Headstock
Manual 3 gear, stepless speed adjustment in the gear, with the servo spindle motor through the belt, gear box to drive the spindle rotation, headstock front assembly manual three-jaw chuck for clamping workpiece.
Gear precision grinding processing; The gear tooth surface is treated by high-frequency quenching, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and impact load.
The external lubricating oil box is used for circulating lubrication of gears and bearings, and low liquid level alarm device is installed in the oil tank.
A button plate is installed on the headboard box, which has the functions of spindle point, feed forward, feed backward and emergency stop.
The gears are machined by precision grinding , gear surface is quenched by high frequency quenching, and the hardness of the tooth surface is HRC48-52, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and shock load.
In order to improve the service life of gears and bearings, lubricating oil is used to circulate lubrication
.
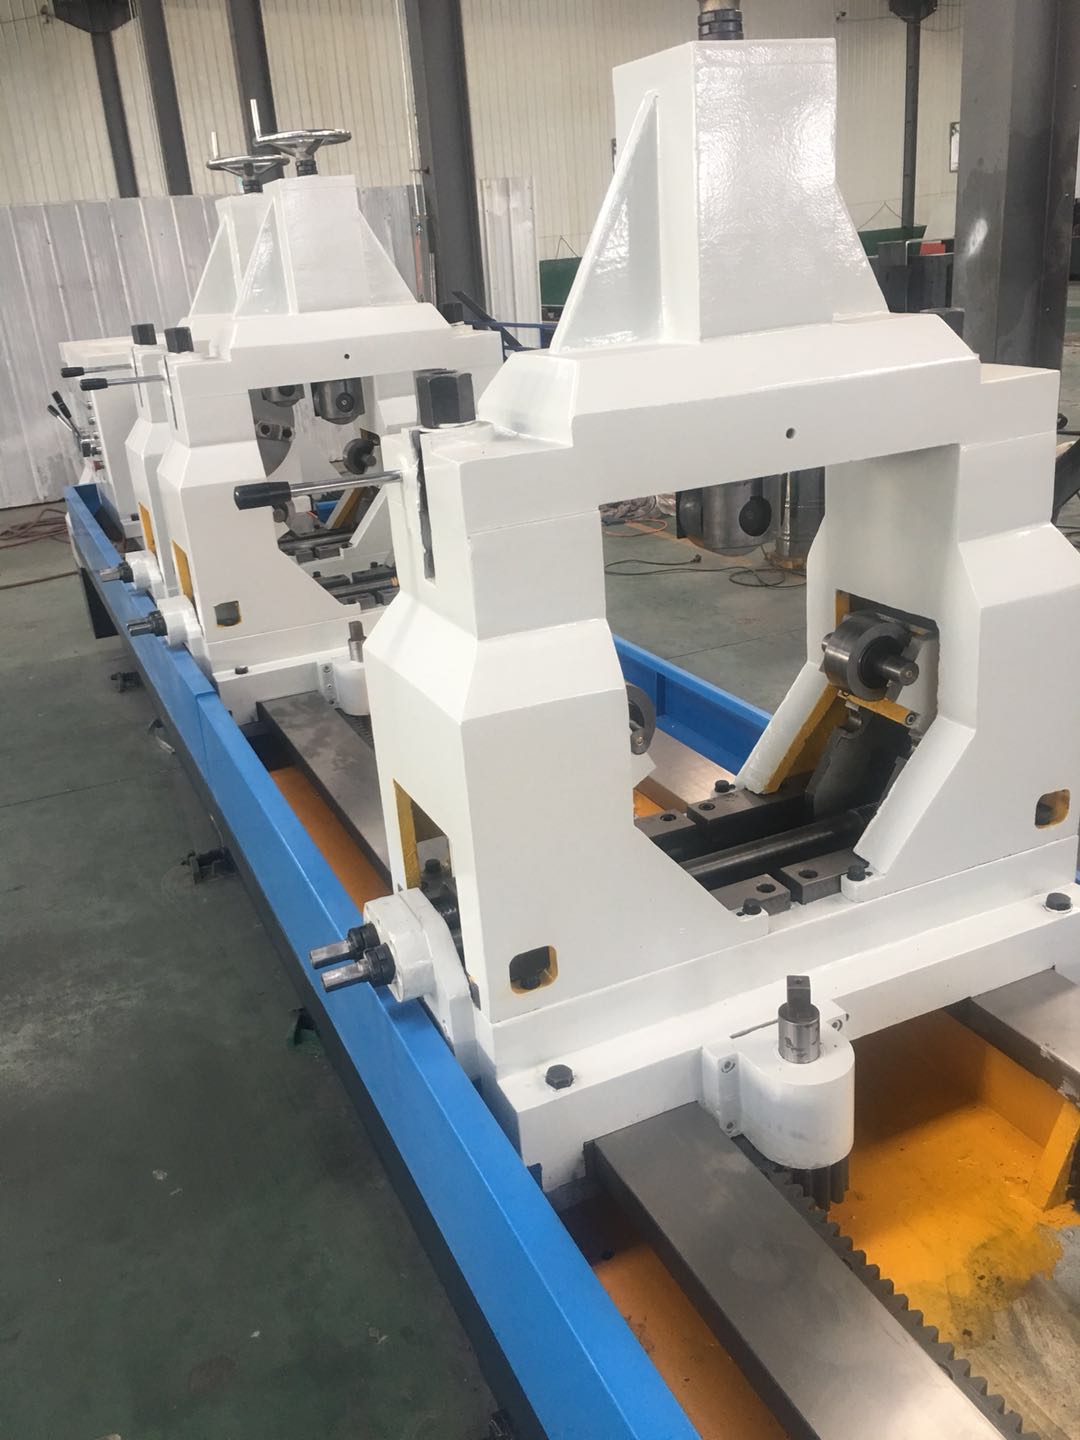
1.3. 7 Center rest
Used for supporting the workpiece; Three-point closed type center rest structure, two rollers below, and one roller on the top; The lateral position of two rollers below is adjusted by screw. The position of center rest on the guide rail could be adjusted through rack and pinion manually.
1.3.8 Oil pressure head
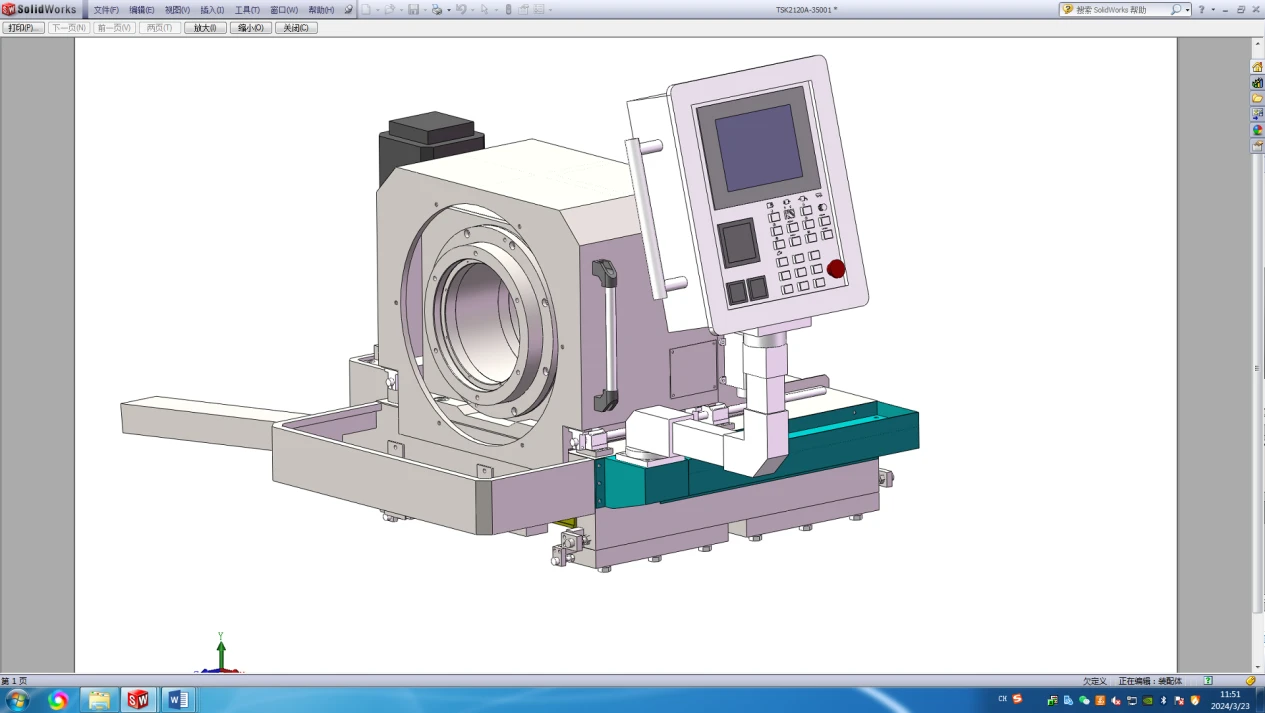
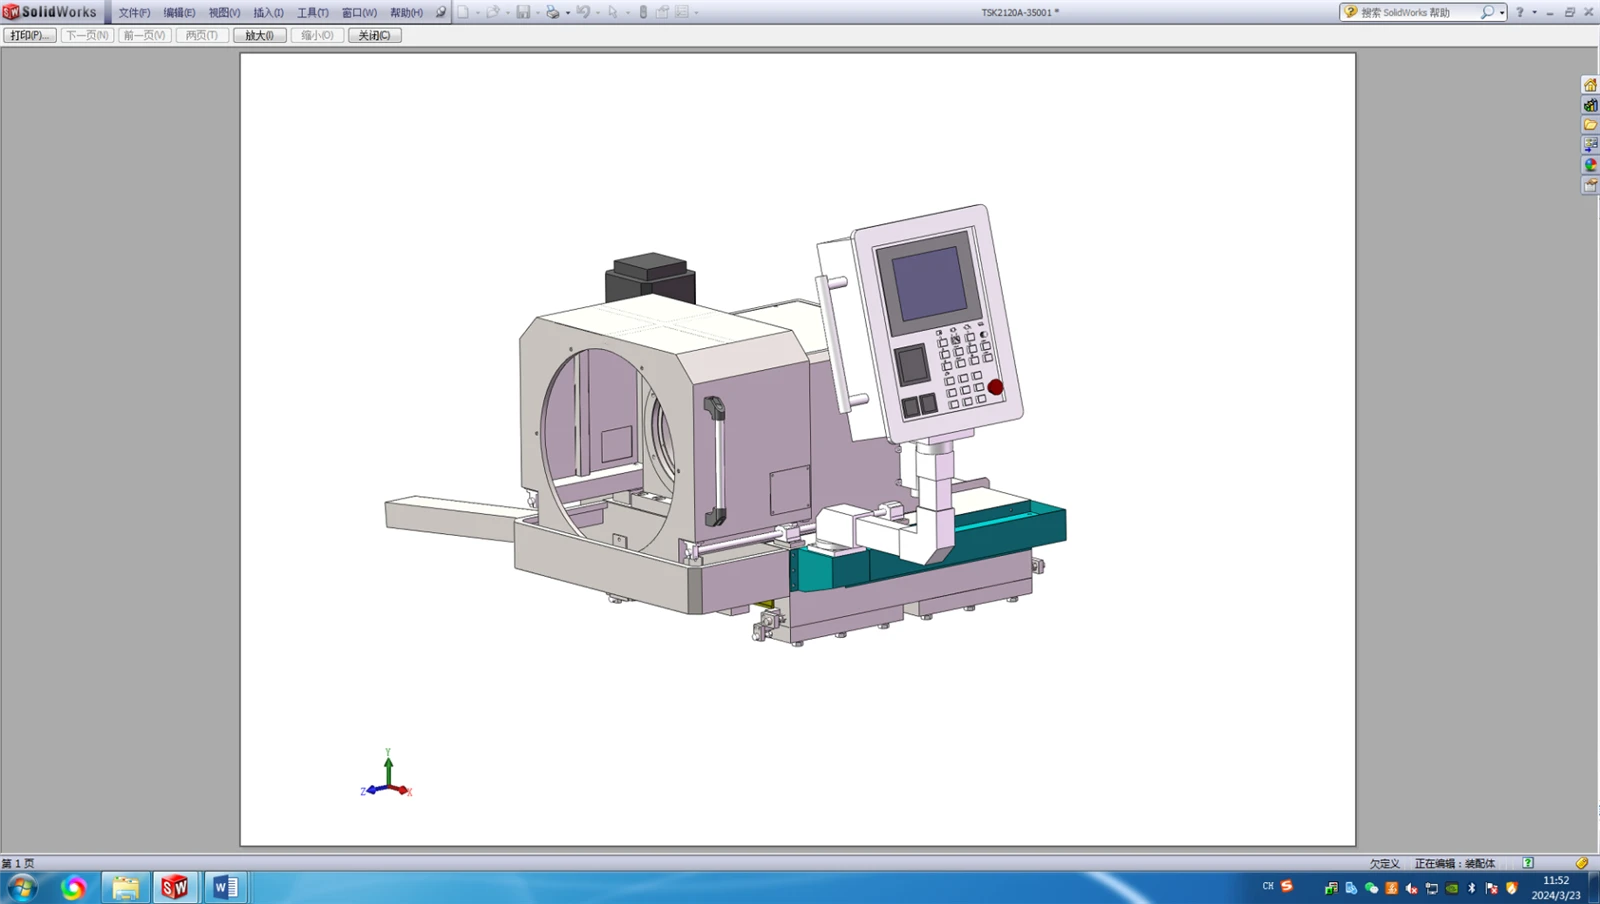
Used for guiding the cutting tool, supplying cutting oil and supporting the workpiece ; Servo motor drives its axial movement to adapt the workpiece with different length, and to tighten and loosen the workpiece .
Servo motor is used to drive the oil pressure head to tighten or loosen the workpiece, with high precision and rigidity;the whole oil pressure head adopts box structure, with high precision and rigidity.
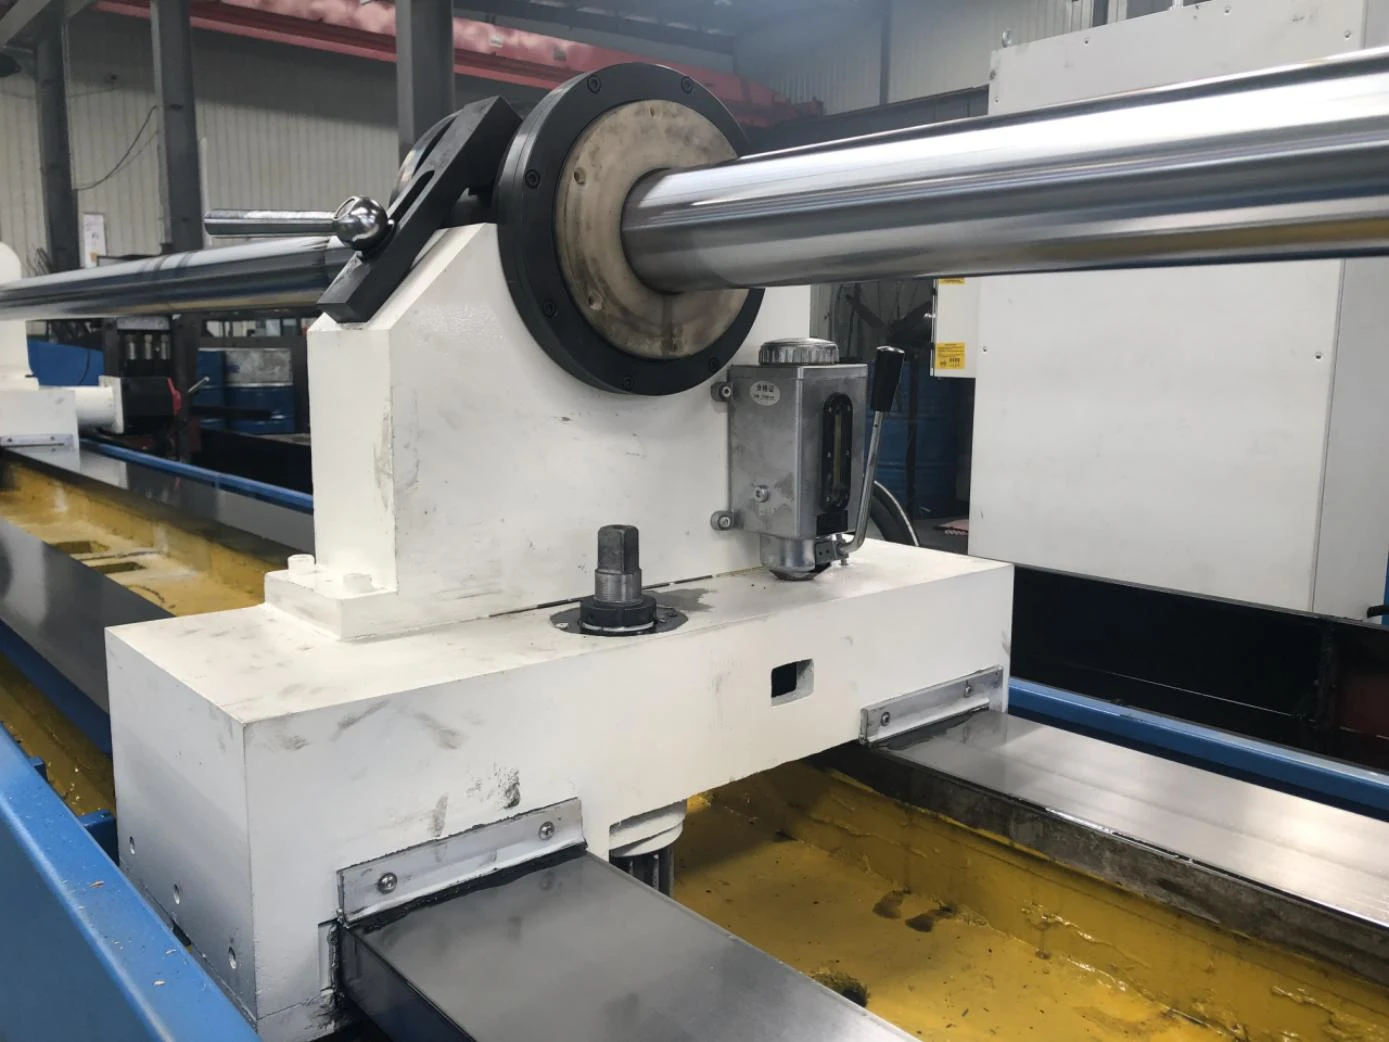
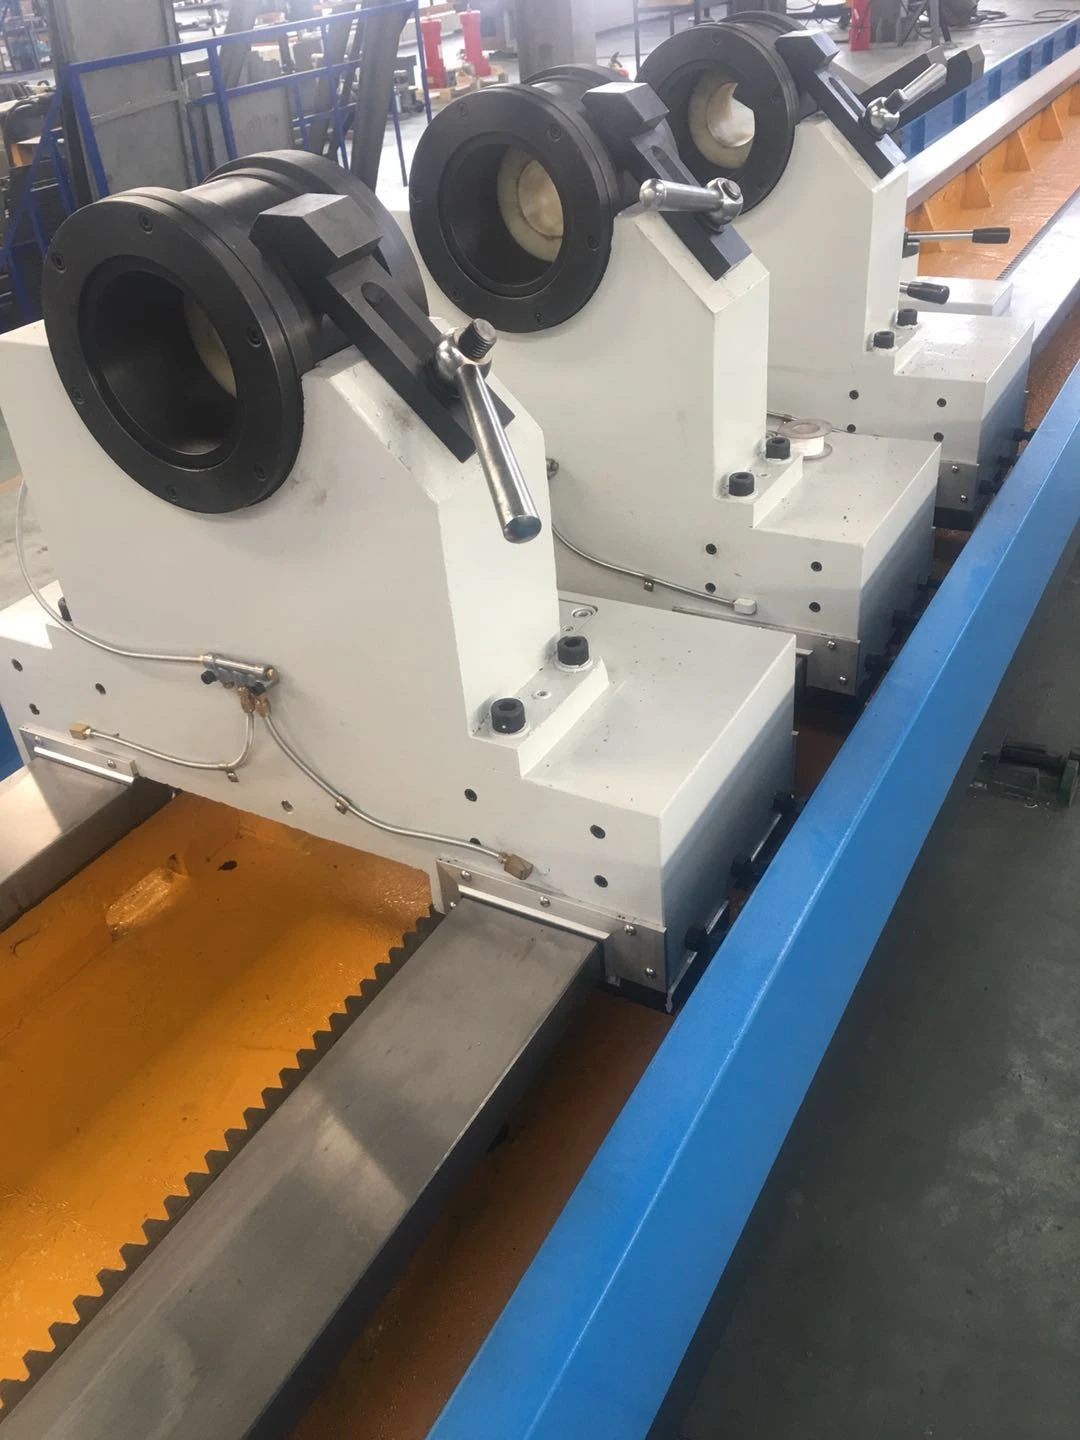
1.3.9 Drill bar support rest
Used for supporting the drill bar ; A high rigidity integral structure is adopted, on which a support sleeve is assembled, which can absorb the shock and vibration produced during machining and so on .
1.3.10 Coolant system :
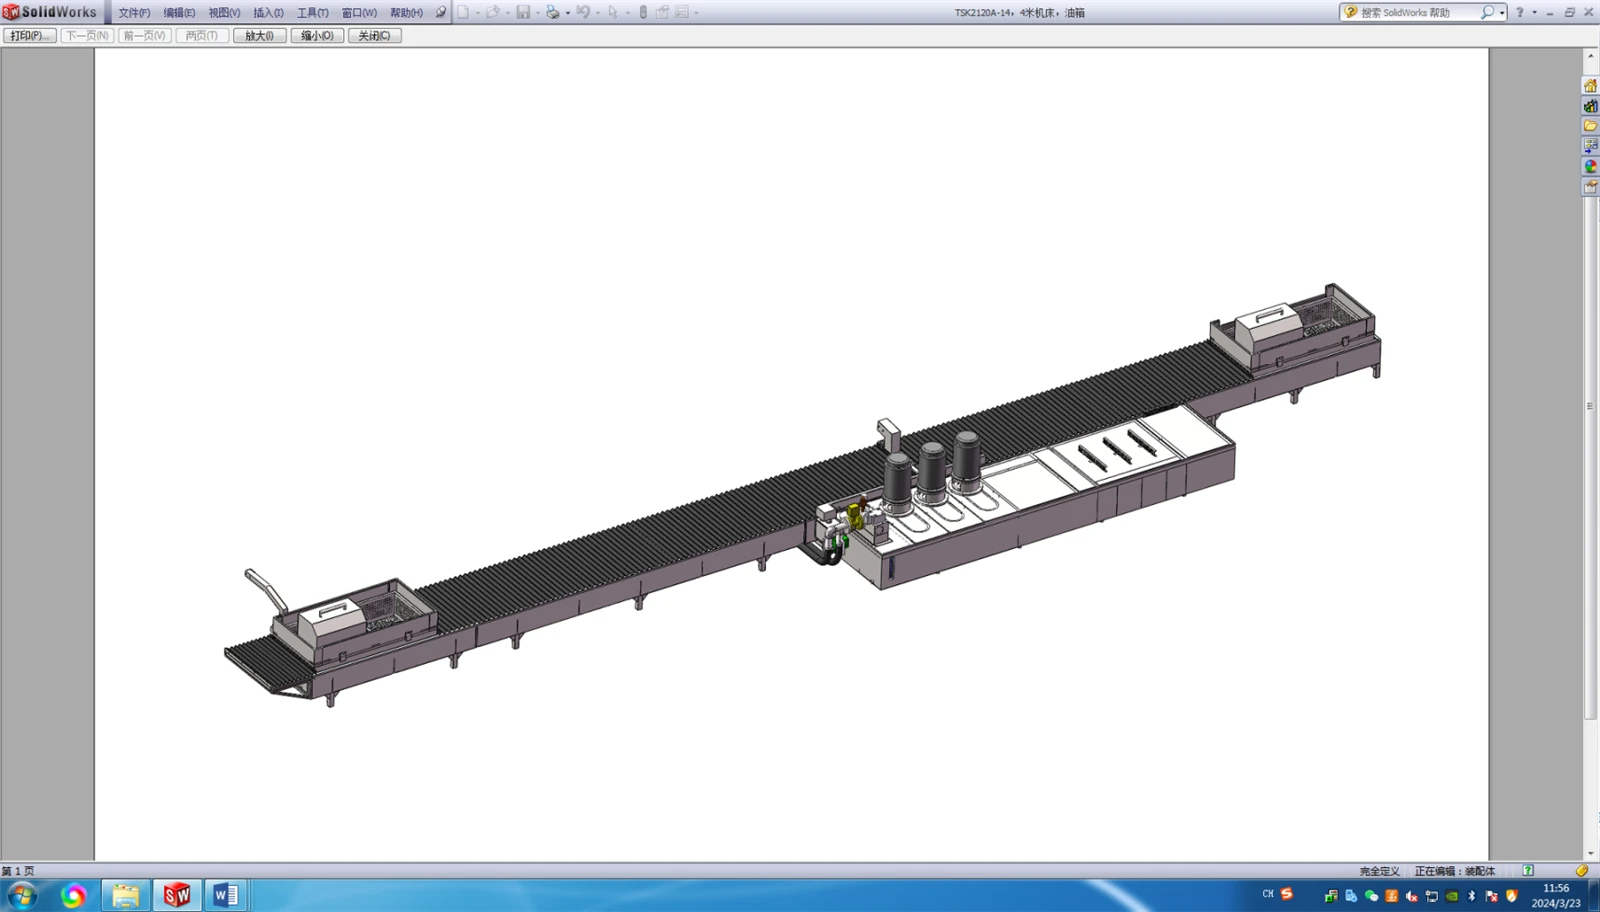
It is mainly composed of cooling pump, chip box, oil tank, etc., which provides enough cutting oil for deep hole processing.
Above ground fuel tank, the fuel tank is fully welded with high-quality steel plate.
A telescopic protective cover is installed between the chip boxes on the fuel tank to cover the fuel tank to prevent sundries from falling into the fuel tank.
The pressure, liquid level, oil temperature and flow rate of cutting oil can be displayed digitally on the control station.
1.3.11 Drill box
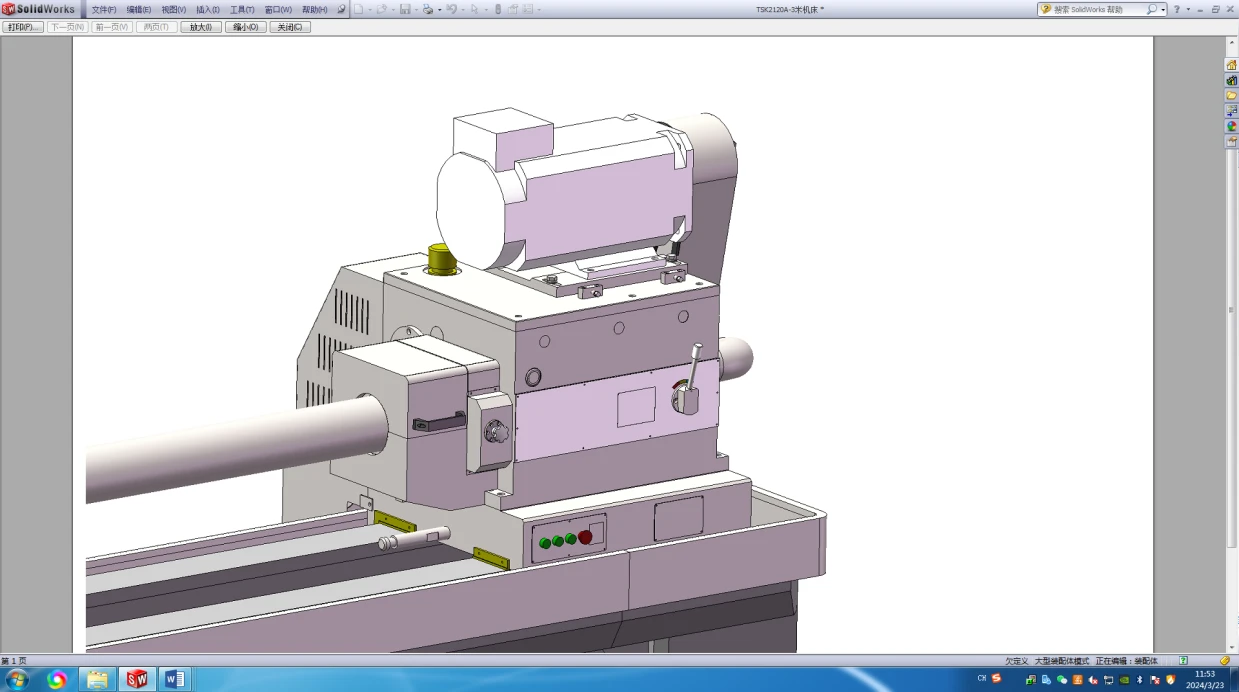
Used to drive tool rotation, mounted on the feed plate.
Manual 3, stepless speed adjustment in the gear, with the servo spindle motor through the belt, belt wheel, gear system to drive the spindle rotation.
The left end of the spindle is equipped with a tool handle connecting sleeve for clamping the tool.
The right end of the spindle is equipped with a chip hopper for discharging chips.
Gear precision grinding processing; The gear tooth surface is treated by high-frequency quenching, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and impact load.
The external lubricating oil box is used for circulating lubrication of gears and bearings, and low liquid level alarm device is installed in the oil tank.
The gears are machined by precision grinding , gear surface is quenched by high frequency quenching, and the hardness of the tooth surface is HRC48-52, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and shock load.
In order to improve the service life of gears and bearings, lubricating oil is used to circulate lubrication.
1.3. 11 Feed pallets
Used to drive the tool to move axially.
The automatic lubrication station is used to lubricate the sliding rail surface at fixed time and quantity.
A push button plate is installed on the supporting plate, which has the functions of punching the main shaft of the drill pipe box, feeding forward, feeding backward, and emergency stop.
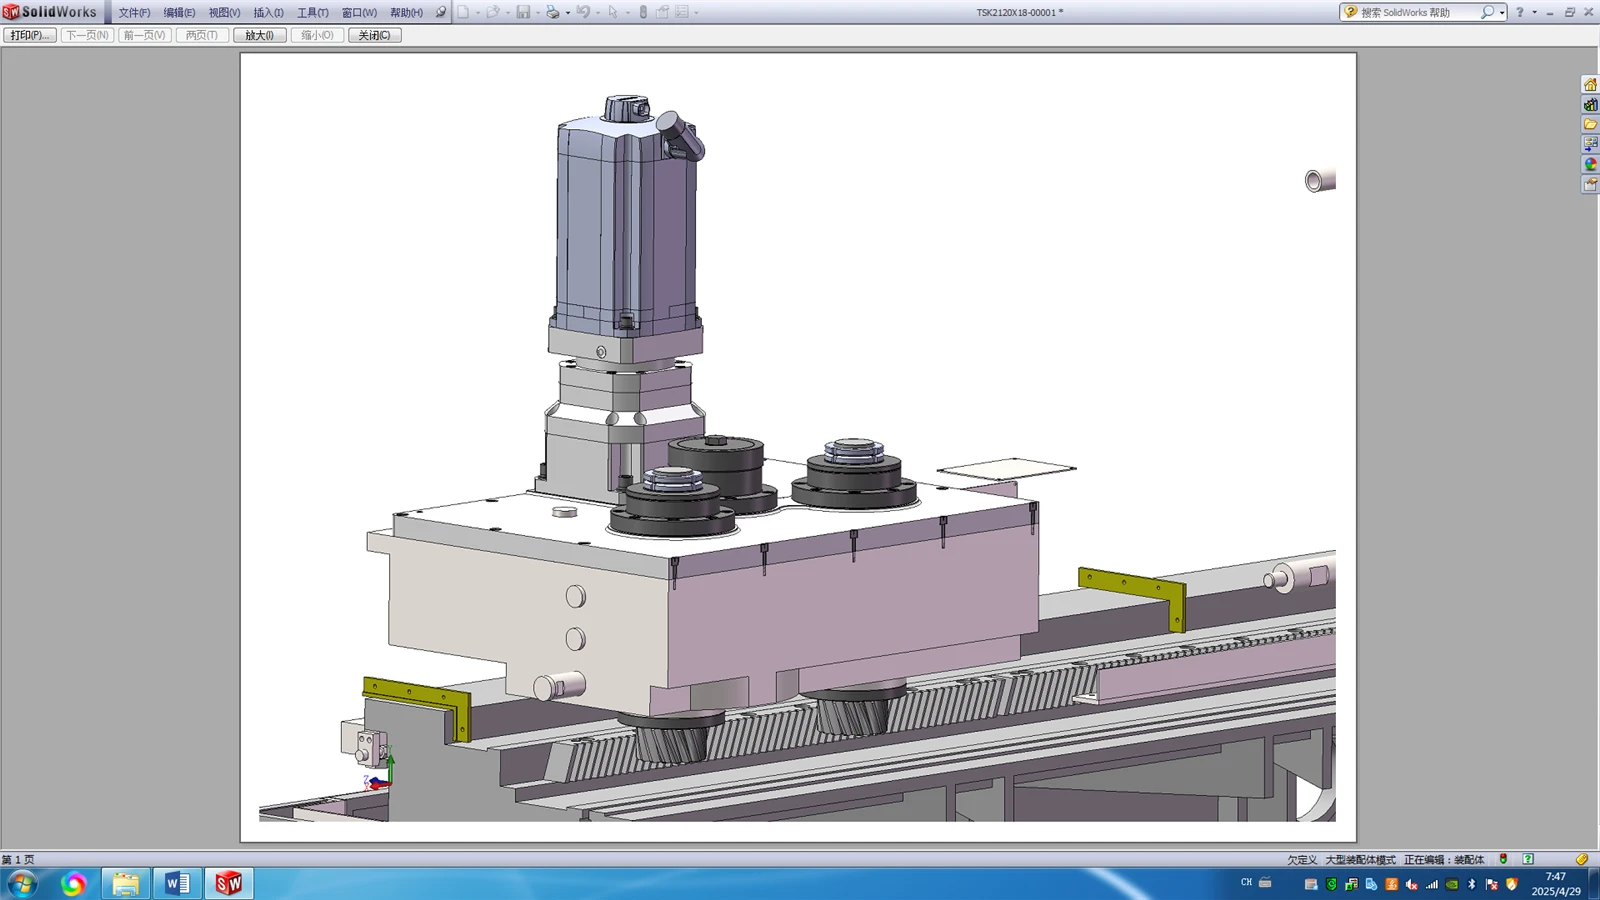
1.3. 12 lubrication system
The sliding guide rail surface of the feed support plate adopts automatic lubrication station for timing and quantitative lubrication, and has the function of low liquid level alarm.
The bearings and gears of the headstock are lubricated by an independent external fuel tank with low liquid level alarm function.
Bearings and gears of drill pipe box are lubricated by an independent external oil tank with low liquid level alarm function.
The lubricator support plate and the cutter holder support plate are lubricated by manual lubrication pump.
1.3. 13 Workpiece brackets
Used for workpiece preposition.
The operator puts the workpiece on the workpiece bracket first, and after the workpiece is clamped and positioned, the workpiece leaves the bracket.
The V-frame on the workpiece bracket is manually raised and lowered using the T-screw.
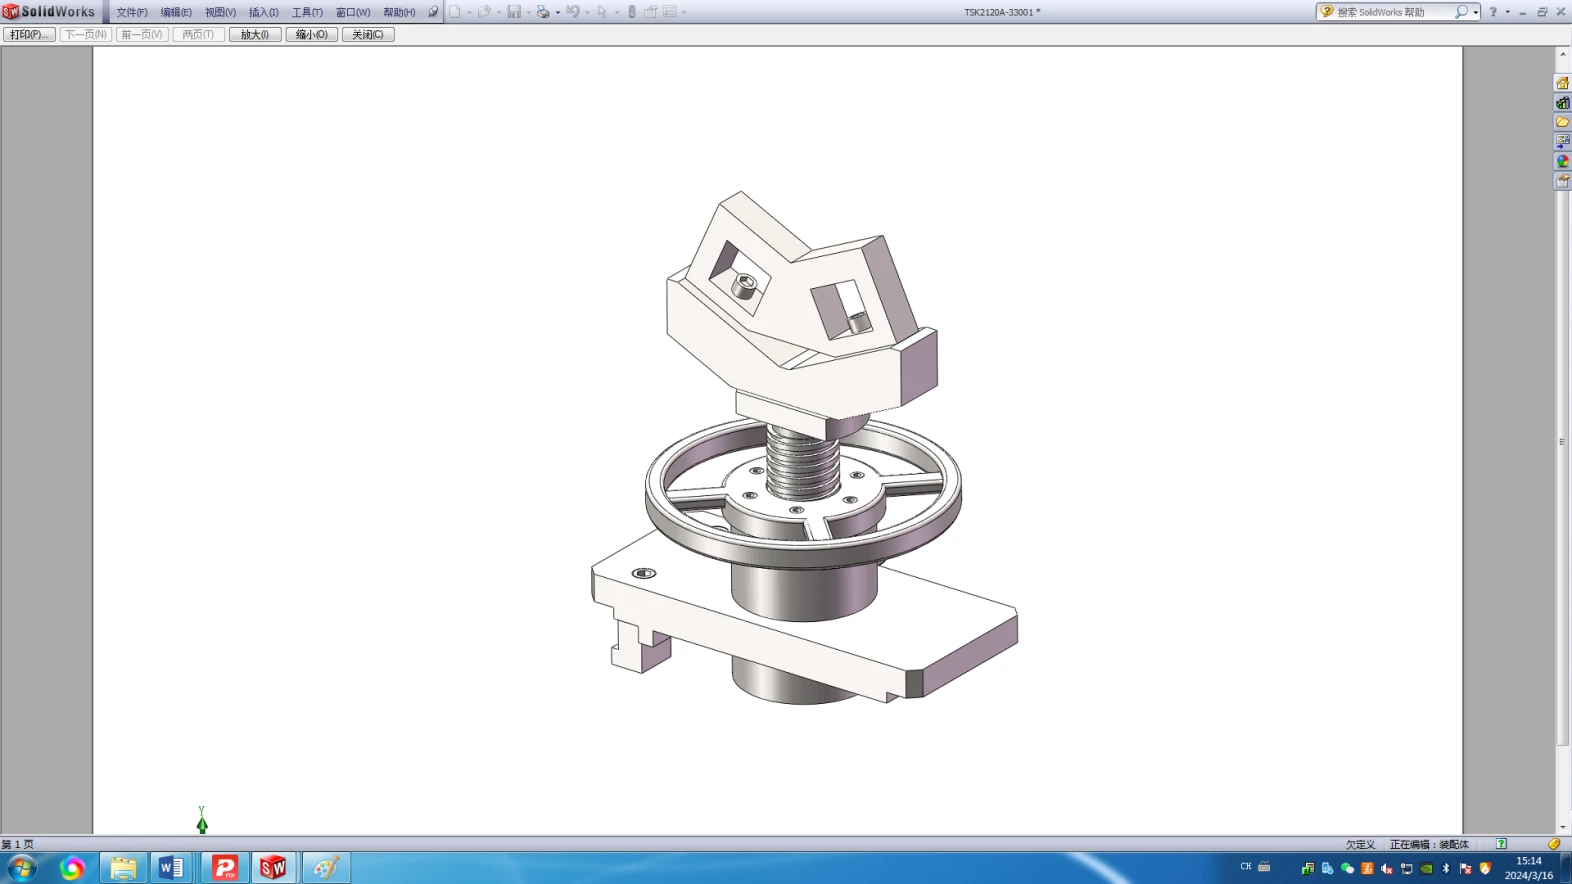
Workpiece bracket diagram
Contact Lean Lee
Whatsapp : 008615153489973
Email :export@dzguanlu.com
Hot Tags: bta deep hole drilling and boring machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like