Latest Products
Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com
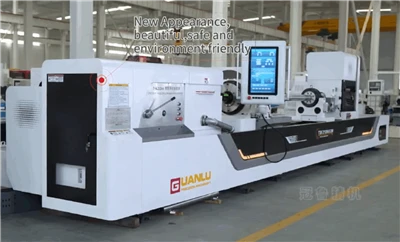

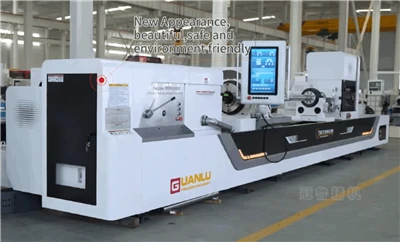


2m BTA Deep Hole Drilling And Boring Machine
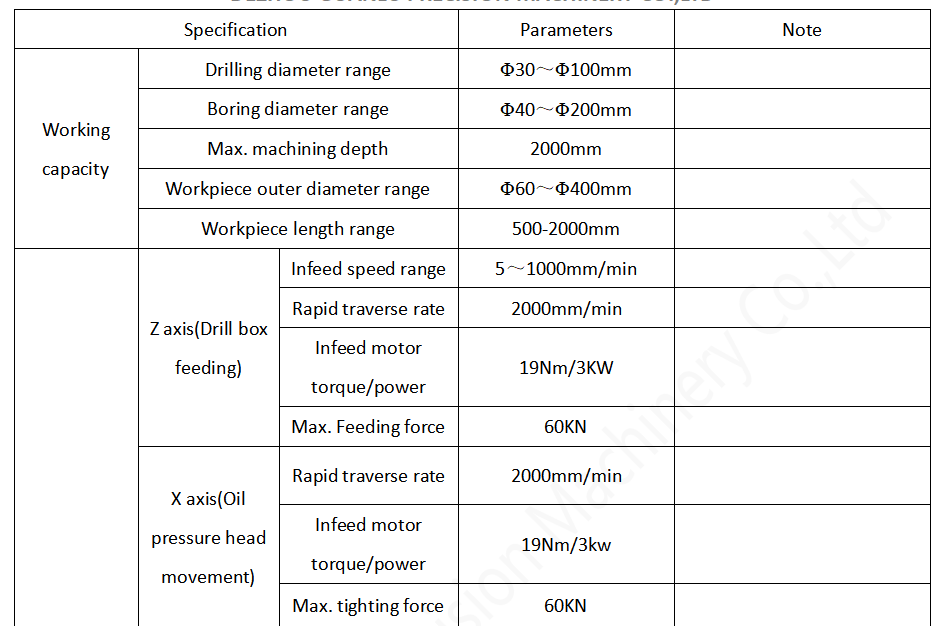
Machine processing range: Solid drilling diameter range :30-100mm Boring diameter range :40-200mm Workpiece OD range :60-400mm
Description
2m BTA deep hole drilling and boring machine
1. Machine Brief:
1.1 Machine processing range:
Solid drilling diameter range :30-100mm
Boring diameter range :40-200mm
Workpiece OD range :60-400mm
1.2 Machine function:BTA drilling, pull boring and push boring.
Drilling:BTA drilling method, chip is discharged backward through the drilling bar.
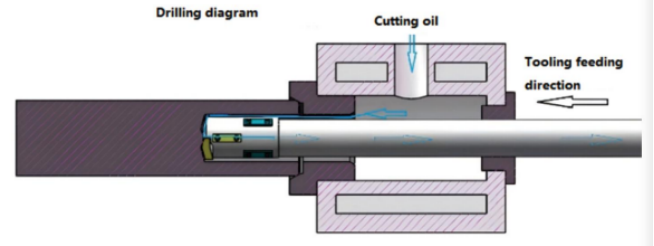
Boring:Push boring method, chip is dispatched forward through the bottom hole of the workpiece.
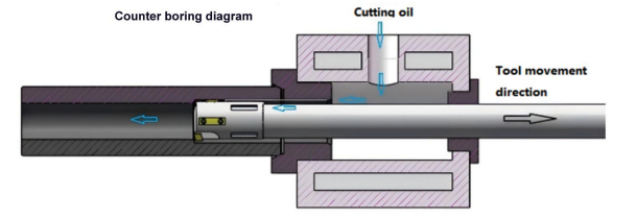
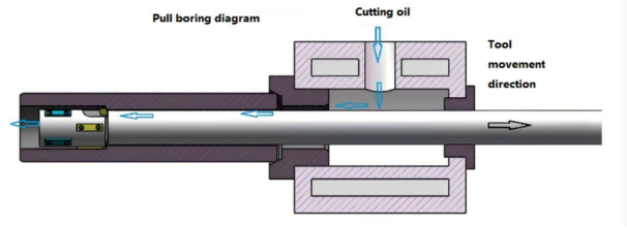
Boring:Pull boring method, the tool is pulled from the far end of the workpiece, and chips are discharged backward through the bottom hole of the workpiece.
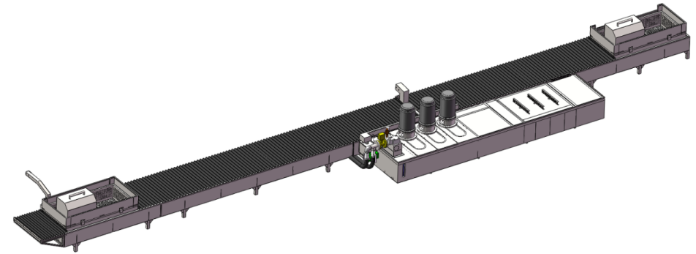
1.3 Machine main structure: 2m BTA deep hole drilling and boring machine
1.3.1 Machine main components:machine bed, headstock, workpiece support rest , oil pressure head, boring bar support rest, drill box, slide rail, rack and pinion,coolant system, FANUC Oi-TF CNC control system, electric box, center rest.
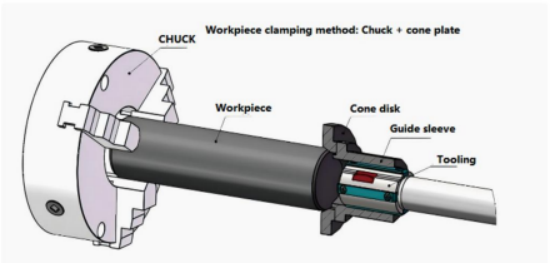
1.3.2 Workpiece clamping method:
The manual three-jaw chuck on the headstock clamps one end of the workpiece, while the cone plate of the oil pressure head automatically presses against the other end.
1.3.3 Machine system: FANUC CNC control system
Z-axis:The longitudinal feed movement of the drill box, the servo motor drives the rack and pinion mechanism through the reduction mechanism.
X-axis: The oil pressure head servos the workpiece, and the servo motor drives the rack and pinion mechanism through the reduction mechanism.
1.3.4 The machine bed, box body, pallet and other basic parts are made of high-quality cast iron precision casting. After the casting is completed, they undergo two aging treatments to eliminate internal stress, stabilize structure and size, and improve mechanical properties.
1.3.5 Machine bed:
The bed body was cast with resin sand and normalized treatment was carried out after casting. The bed body adopts a split structure, which is assembled together by high-strength bolts and positioned by conical pins.
Adopt double rectangular sliding guide, precision grinding, high hardness of guide surface quenching.
The bed is equipped with a bevel rack for the tool feed drive. The rack is precision machined and quenched. The machine tool has large bearing capacity, rigid foot and stable transmission.
V-shaped inclined bar is arranged inside the bed body, which has large support strength and is not easy to deform. The outer wall of the bed directly supports the guide rail, the guide rail can withstand large cutting force, the rigidity of the guide rail is good, and the processing process is not easy to deform and shake, which is conducive to improving the processing quality and efficiency of the machine tool.
The oil return tank is cast around the bed body, and the oil baffle is installed on the return oil tank, and the cutting oil on the bed body automatically returns to the cooling tank.
1.3.6 Headstock:
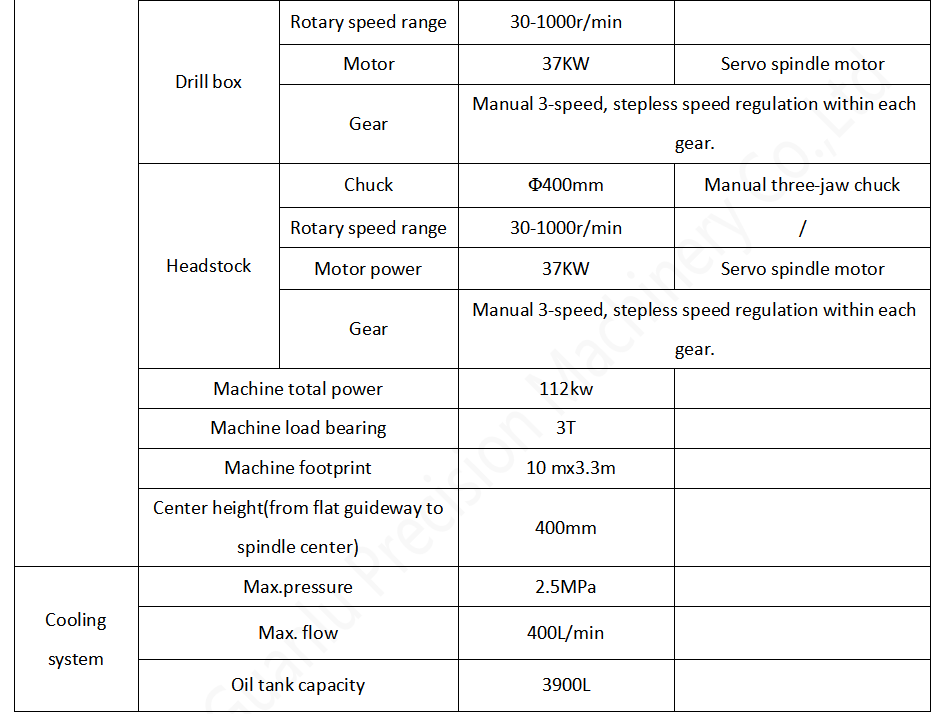
The headstock is used to drive the workpiece to rotate and is fixed on the left end of the bed. It features manual 3-speed with stepless speed regulation within each gear. A servo spindle motor drives the spindle to rotate through a belt and gearbox. A manual three-jaw chuck is mounted on the front end of the headstock for clamping the workpiece.
The gears are manufactured by precision grinding. The gear tooth surfaces are high-frequency quenched, so that the gears achieve high strength, high hardness, high wear resistance, and high fatigue limit, enabling them to withstand relatively large alternating loads and impact loads.
An external lubricating oil tank provides circulating lubrication for the gears and bearings. A low liquid level alarm device is installed inside the oil tank.
A button panel is mounted on the headstock body, providing functions such as spindle jog, feed forward, feed backward, and emergency stop.
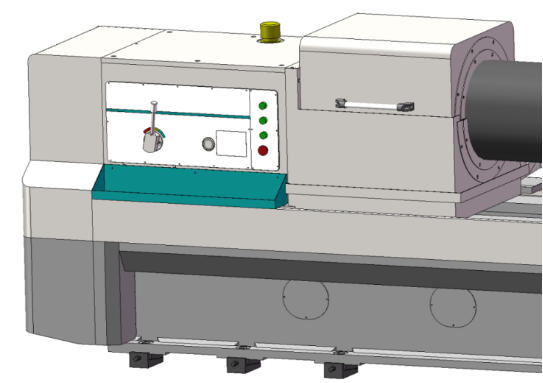
Headstock appearance sketch
1.3.7 Oil pressure head:Used for tool guide, tool oil supply, tool bar support.
The servo motor is used to drive the axial movement of the workpiece to adapt to the processing of different lengths of the workpiece, and to tighten and loosen the workpiece. The servo motor can operate in torque mode or position mode.
The oil pressure head rotary bearing is installed inside the oil receiver body, which has good rigidity and high rotary accuracy.
The rotary seal is installed on the outside of the right end of the oil receiver body for easy maintenance.
The right end of the oil pressure head is equipped with a tool bar support sleeve for supporting the tool bar.
The left end of the oil pressure head is installed with a guide sleeve, a cone and an oil baffle. The cone is used for positioning the workpiece, and the guide sleeve is used for guiding the tool.
The oil blocking device is a push-pull structure, and the oil box is installed at the lower part of the oil blocking device to make the cutting oil flow back to the oil tank.
1.3.8 Drill box
The drill box is used to drive the tool to rotate and is mounted on the feed carriage. It features manual 3-speed with stepless speed regulation within each gear. A servo spindle motor drives the spindle to rotate through a belt, pulleys, and gear train.
A toolholder adapter sleeve is assembled on the left end of the spindle for clamping the tool. A chip discharge hopper is installed on the right end of the spindle to discharge chips.
The gears are manufactured by precision grinding. The gear tooth surfaces are high-frequency quenched, so that the gears achieve high strength, high hardness, high wear resistance, and high fatigue limit, enabling them to withstand relatively large alternating loads and impact loads.
An external lubricating oil tank provides circulating lubrication for the gears and bearings. A low liquid level alarm device is installed inside the oil tank.
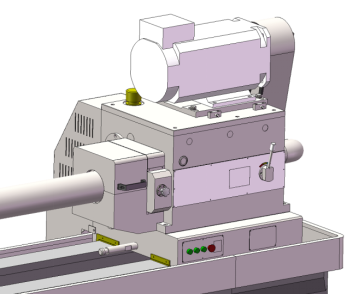
Drill box appearance sketch
1.3.9 Drill bar support rest:
Used to support the tool bar;
The high rigidity of the integral structure, which is equipped with support sleeve, can absorb the impact of the processing process, shake and so on.
Install the automatic hanging mechanism, the feed plate can automatically pull the tool bar support back to the initial position when the tool is withdrawn.
1.3.10 Coolant system:
It is mainly composed of cooling pump, chip box, oil tank, etc., to provide enough cutting oil for deep hole processing.
Above ground oil tank, the oil tank adopts high quality steel plate full welding treatment.
A retractable protective cover is installed between the chip receiving boxes on the oil tank to cover the oil tank to avoid debris falling into the oil tank.
Cutting oil pressure, liquid level, oil temperature, flow, can be digitally displayed on the control station.
2. Machine main parameters: 2m BTA deep hole drilling and boring machine
https://www.guanludrilling.com/gun-drilling-machines/double-spindle-cnc-gun-drilling-machine.html
More details, please feel free to contact me!
Sunny Lee: +86 15153489925; dz@dzguanlu.com
Hot Tags: 2m bta deep hole drilling and boring machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like