Latest Products

Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com
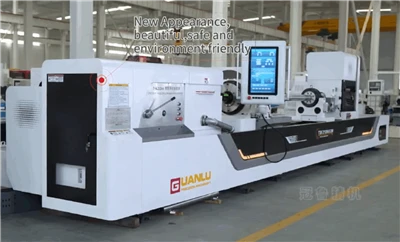
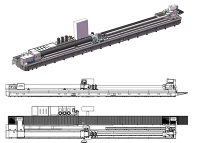
ZSK2106F×2 Compound CNC Deep Hole Drilling Machine
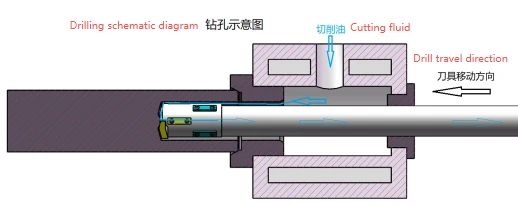
1.Machine Overview 1.1 Drilling method: Gun drill (external chip removal) and BTA (internal chip removal) BTA drilling: Cutting oil is fed to the cutting tool through the gap between the oil feeder, the drill tube and the hole wall. The cutting fluid carries chips out via the inner bore of the drill tube. The workpiece and the cutting tool rotate relative to each other.
Description
1.Machine Overview
1.1 Drilling method: Gun drill (external chip removal) and BTA (internal chip removal)
BTA drilling: Cutting oil is fed to the cutting tool through the gap between the oil feeder, the drill tube and the hole wall. The cutting fluid carries chips out via the inner bore of the drill tube. The workpiece and the cutting tool rotate relative to each other.
Gun drill method (external chip removal): Cutting oil is supplied through the rotary joint at the rear end of the spindle of the drill head box, flows through the inner bore of the drill tube to the cutting zone, and carries chips out through the gap between the V-groove of the drill tube and the hole wall.
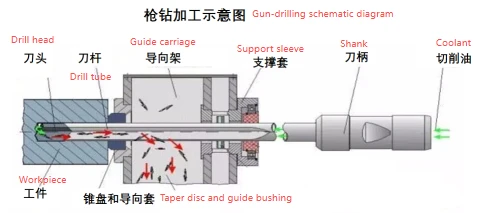
One spindle is shared for both gun-drilling and BTA processes. To switch between gun-drilling and BTA modes, manual replacement of cutting tools and accessories as well as oil circuit switching are required, enabling conversion between the two machining methods.
Machine operating modes: Workpiece rotation, tool rotation, tool feed.
1.2 Machining Range
Gun-drilling range: Ø6–Ø50 mm
BTA drilling range: Ø16–Ø500 mm
Maximum drilling depth: 2500 mm
Number of spindles: 2
2. Main Machine Structure
2.3.1 Main Components
Machine bed, headstock, oil feeder, tool bar support, drill head box, cooling system, control system, electrical cabinet, workpiece support, steady rest, etc.
2.3.2 Workpiece Clamping
Taper discs are mounted on the headstock and oil feeder respectively. By means of chamfers on both ends of the workpiece, the workpiece is automatically pressed and positioned.
2.3.3 Machine Control System
Control system: SIEMENS-828D Z-axis: Longitudinal feed motion of the drill head box, driven by a servo motor through a reduction unit to actuate the rack-and-pinion mechanism. Main control functions: Workpiece rotation, tool rotation, tool feed, cooling system, etc.
2.3.4 Base components such as boxes, machine bed and slide plate are precision-cast from high-grade cast iron. Two stress-relieving treatments are carried out after casting to eliminate internal stress, stabilize microstructure and dimensions, and improve mechanical properties.
2.3.5 Machine Bed
The machine bed is resin-sand cast and normalized after casting. It adopts a split structure, assembled with high-strength bolts and positioned by taper pins.
The tool bed is equipped with double rectangular slideways, precision-ground with high surface hardness after quenching. A ball screw is fitted inside the tool bed for tool feed transmission. A rack is mounted on the side of the tool bed for manual adjustment of the tool bar support.
Ball linear guides are installed on the workpiece bed, together with a worktable machined with T-slots. The headstock and steady rest can be moved manually along the linear guides for quick and convenient positioning.
V-shaped inclined ribs are arranged inside the bed to provide high supporting stiffness and resist deformation. The outer wall of the bed directly supports the slideways, enabling the slideways to withstand heavy cutting forces with high rigidity. Minimal deformation and vibration occur during machining, which helps improve machining quality and efficiency.
Oil return grooves are cast around the bed with oil splash guards fitted on top. Cutting fluid from the bed flows back automatically into the coolant tank.
2.3.6 Headstock
It drives workpiece rotation and is mounted on the linear guides of the workpiece bed.
The main motor drives the spindle via belts and a reduction gearbox to provide stepless speed regulation. A taper disc is fitted at the front end of the headstock for workpiece clamping.
The entire headstock can be manually moved axially along the linear guides of the workpiece bed and locked onto the worktable by clamping blocks once positioned.
One motor drives both spindles at a fixed rotational speed.
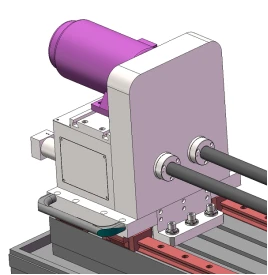
2.3.7 Oil pressure head
It serves for tool guiding, cutting fluid supply, drill tube support and chip removal.
The oil pressure head is mounted at the middle section of the machine bed. Its guide bushing moves axially under hydraulic control to clamp or release the workpiece.
A drill tube support sleeve is fitted on the right-hand side of the oil feeder to support the drill tube.
A guide bushing and a taper disc are installed on the left-hand side. The taper disc positions the workpiece while the guide bushing provides guidance for the cutting tool.
For gun-drilling operations, the oil feeder enables chip removal. For BTA drilling operations, the oil feeder supplies cutting fluid to the tool.
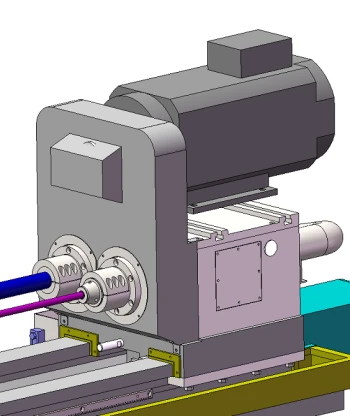
2.3.8 Drill Head Box
It drives the rotation of cutting tools and is mounted on the feed slide plate.
A servo spindle motor drives the spindle through belts and pulleys for stepless speed regulation.
A shank adapter is fitted at the left end of the spindle for tool clamping.
For BTA machining, a chip chute is installed at the right end of the spindle to discharge chips. For gun-drilling machining, a rotary joint is fitted at the right end of the spindle to supply cutting fluid to the tool.
The main motor is front-mounted to drive spindle rotation. The rear end of the motor is kept away from the shank adapter. This prevents oil ingress into the motor, extends service life and facilitates tool changing.
One motor drives both spindles with stepless speed regulation.
2.3.9 Tool Bar Support
It is used to support the tool bar. It adopts a high-rigidity monolithic structure fitted with support sleeves, which can absorb shocks, vibrations and other disturbances generated during machining. An automatic pull-back mechanism is installed. During tool retraction, the feed carriage can automatically pull the tool bar support back to its home position. Meanwhile, manual adjusting gears are mounted on the support, allowing manual adjustment of the tool bar support position along the machine bed.
2.3.10 Cooling System
It mainly consists of a cooling pump, chip conveyor, oil chiller, filter unit, oil tank and other components, supplying sufficient cutting oil for deep hole machining. This is an above-ground oil tank fabricated from high-quality steel plates with full penetration welding.
Chip conveyor: It removes metal chips and achieves primary separation of oil and chips.
Oil chiller: It keeps oil temperature within a reasonable range. The oil chiller starts automatically when the oil temperature exceeds the upper set limit and stops automatically when the oil temperature drops below the lower set limit.
Filter unit: It adopts paper band filtration with automatic paper feeding function to improve the cleanliness of cutting oil.
The pressure, liquid level, temperature and flow rate of cutting oil are digitally displayed on the operator station.
2.3.11 Feed Carriage
It is used to drive the tool for axial movement. An automatic lubrication station provides timed and quantitative lubrication for the sliding guide surfaces. A button panel is fitted on the carriage, featuring functions including inching of the spindle of the drill box, forward feed, backward feed and emergency stop.
2.3.12 Lubrication System
The sliding guide surfaces of the feed carriage are lubricated by an automatic lubrication station with timed and quantitative oil supply, equipped with a low liquid level alarm. Bearings of the headstock are lubricated by an automatic lubrication station with timed and quantitative oil supply, equipped with a low liquid level alarm. Bearings of the drill box are lubricated by an automatic lubrication station with timed and quantitative oil supply, equipped with a low liquid level alarm. The tool bar support carriage is lubricated by a manual lubrication pump.
2.3.13 Workpiece Rest
It is used for pre-positioning of the workpiece. The operator places the workpiece on the workpiece rest first. Once the workpiece is clamped and positioned, it will separate from the rest.
3.Main Parameters of Machine Tool
Technical Specifications
Working Range
Drilling diameter range: Gun drill Φ6~Φ50mm; BTA Φ16~Φ50mm
Workpiece length: 400-2500mm
Maximum machining depth: 2500mm
Workpiece outer diameter range: Φ30~Φ200mm
Number of spindles: 2 Spindle center distance: 280mm
Machine Tool Performance
Z-axis feed speed range: 5~3000mm/min
Z-axis rapid traverse speed: 3000mm/min
Z-axis servo motor: 27Nm / 4.3KW
Drill box maximum rotational speed: 2500r/min, stepless speed regulation
Drill box motor power: 45KW, servo main motor
Headstock rotational speed: 20r/min, fixed speed
Headstock motor power: 3.7KW, standard motor
Cooling system maximum pressure: Gun drill 8MPa, adjustable; BTA 4MPa, adjustable
Cooling system maximum flow rate: 300L/min, adjustable
Oil tank capacity: 3000 Liters
Other parameters
Height from spindle center to top surface of guideway: 240mm
Total installed power of machine tool (approx.): 90KW
Machine tool floor space: 9m × 3.5m
4.Contact Me:
Email:sale@dzgaunlu.com
Whatsapp/Wechat:+8613853423246
5.Other Machine
Hot Tags: zsk2106f×2 compound cnc deep hole drilling machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like