Latest Products

Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com
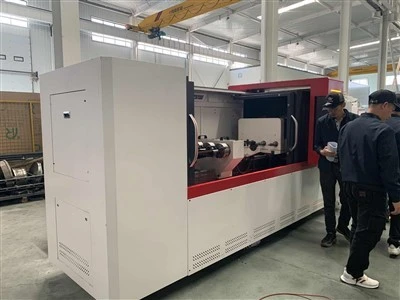
ZSK2202DZ×500 CNC Deep Hole Drilling Machine
Machine Overview This machine is a high-efficiency, high-precision and highly automated CNC deep hole drilling machine for small-diameter holes adopting the external chip removal drilling method (gun drilling method). It can achieve the machining accuracy and surface roughness that normally require sequential drilling, reaming and finishing operations in one continuous drilling pass. It is capable of drilling equal-diameter deep holes, as well as blind holes and stepped holes. Designed mainly for deep hole machining of workpieces with irregular profiles, this machine adopts a single-spindle configuration for processing one workpiece at a time. Gun drilling mode: internal coolant supply and external chip removal. Cutting fluid flows through the rotary union at the rear end of the spindle in the drill box, the inner bore of the drill box spindle and the inner bore of the tool bar to reach the cutting edge. The cutting fluid carries chips through the V-shaped groove on the outer surface of the tool bar into the guide bushing assembly, and then to the chip conveyor.
Description
1.Machine Overview
1.1Machine Application
This machine is a high-efficiency, high-precision and highly automated CNC deep hole drilling machine for small-diameter holes adopting the external chip removal drilling method (gun drilling method). It can achieve the machining accuracy and surface roughness that normally require sequential drilling, reaming and finishing operations in one continuous drilling pass.
It is capable of drilling equal-diameter deep holes, as well as blind holes and stepped holes.
Designed mainly for deep hole machining of workpieces with irregular profiles, this machine adopts a single-spindle configuration for processing one workpiece at a time.
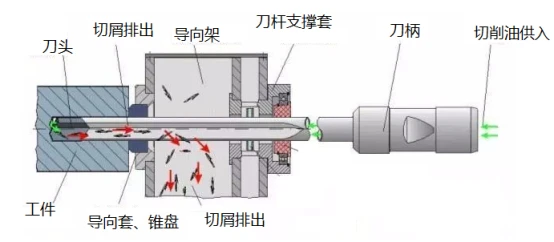
Gun drilling mode: internal coolant supply and external chip removal. Cutting fluid flows through the rotary union at the rear end of the spindle in the drill box, the inner bore of the drill box spindle and the inner bore of the tool bar to reach the cutting edge. The cutting fluid carries chips through the V-shaped groove on the outer surface of the tool bar into the guide bushing assembly, and then to the chip conveyor.
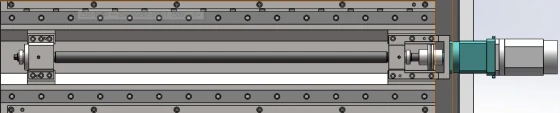
Linear ball guides are adopted for the machine.
1.2 CNC System: KND
1.3 Machine Guarding
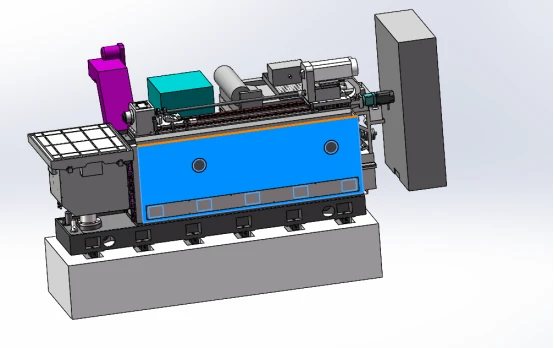
The machine is fitted with newly custom-designed guarding to match the machine's appearance and operational requirements, with zero oil leakage. A CNC control panel is integrated on the guarding, which accommodates detection units for flow adjustment, machine pressure monitoring and other parameters, with all readings displayed on the panel.
1.4 Drill Box
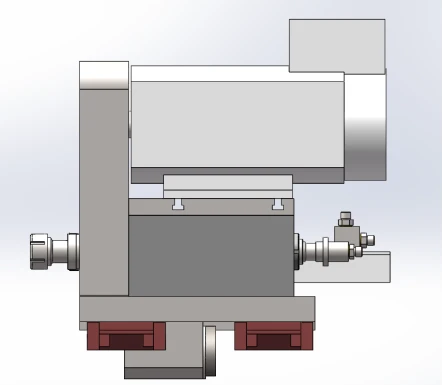
The spindle rotation is driven by a servo main motor via timing belts and timing pulleys to provide stepless speed regulation. The spindle speed range is 500~5000 r/min, and the main motor power is 5.5 kW. A Korean rotary union is mounted at the rear end of the spindle to deliver stable coolant supply for deep hole machining and ensure smooth cutting. Linear ball guides are used for the travel of the drill box to extend the service life of the machine. Angular contact ball bearings are fitted inside the drill box spindle to guarantee stable cutting performance. A spring collet is equipped on the drill box for clamping gun drill tools.
1.5 Machine Bed
The machine bed is of three-side enclosed structure with rationally arranged reinforcing ribs. Made of high-grade cast iron HT300, it features sufficient rigidity to meet the requirements of high-speed cutting.
1.6 Tool Feed System (Z-Axis): Used to drive the tool for feeding motion. The ball screw is driven by a servo motor to realize tool feeding movement. The nut on the ball screw is of double-nut construction, lubricated at fixed time and quantity by an automatic lubrication station. Special screw bearings are fitted at both ends of the screw, adopting a bearing arrangement fixed at one end and pre-tensioned at the other end. The Z-axis servo feed system consists of a servo motor, servo reducer and ball screw.
1.7 Drill Support 2 sets, supporting a maximum hole length-to-diameter ratio of 100:1.
1.8 X-Axis (with Worktable)
The T-slot worktable of the X-axis is made of high-grade cast iron HT300. The X-axis adopts a drive configuration combining linear ball guides and ball screws for reciprocating travel of the T-slot worktable. The X-axis servo feed system consists of a servo motor, servo reducer and ball screw. Dimensions of the T-slot worktable: 500 mm × 500 mm
1.9 Coolant System Components: Chip Conveyor with Chain Plate, Circulating Pump, Paper Band Filter, Oil Chiller, Pump Unit, Level Sensor, Flow Sensor, Pressure Sensor, Temperature Sensor, Oil Tank.
Floor-mounted oil tank, fully welded from high-quality steel plates. Various sensors are installed on the coolant system. Liquid level, oil temperature, flow rate and pressure values are displayed on the indicators.
Pump Unit: One set of variable frequency pump. The output flow of the pump is adjusted by changing the motor speed. A manual relief valve is fitted at the pump outlet to regulate the output pressure.
Chain Plate Chip Conveyor: Conveys chips into the chip trolley, while cutting fluid drains into the dirty oil tank.
Circulating Pump: Delivers cutting fluid from the dirty oil tank to the filter.
Paper Band Filter: Removes contaminants from the cutting fluid coming from the dirty oil tank, equipped with automatic paper feeding function.
Oil Chiller: Cools the cutting fluid and starts/stops automatically according to the preset upper and lower limits of oil temperature.
1.10 Guide Bracket
The guide bracket is provided with an internal cavity to ensure smooth chip evacuation without clogging. A guide bushing is mounted at its left end for drill guidance, sealing and chip removal. A drill rod support sleeve is installed at the right end of the guide bracket to support the drill rod and improve its rigidity. The guide bushing inside the guide bracket can rotate together with the workpiece. When machining workpieces with different hole diameters, the matching guide bushing needs to be replaced. After the machine runs for a period of time, the inner bore of the guide bushing will wear to a certain extent. It shall be replaced with a new one once it fails to meet the precision requirements of the workpiece. The guide bracket adopts a pneumatic system to clamp the workpiece.
1.11 Lubrication System
The linear guide sliders and ball screw nuts for the travel of the drill box and X-axis are lubricated at fixed time and quantity by an automatic lubrication station.
2.Main Machine Parameters
Technical Specifications
Working Range
Drilling diameter range: Φ3~Φ20 mm
Maximum workpiece length: 500 mm
Maximum machining depth: 500 mm Number of spindles: 1
Machine Performance
Z-axis (Tool Feed) Tool feed speed range: 5~500 mm/min
Rapid traverse speed: 5000 mm/min
Motor torque: 10 Nm
Ball screw specification: Φ50×10
Linear ball guide size: 45
X-axis Travel: 500 mm
Rapid traverse speed: 3000 mm/min
Motor torque: 15 Nm
Ball screw specification: Φ50×10
Linear ball guide size: 45
Drill Box
Maximum spindle speed: 5000 r/min, stepless speed regulation
Main motor power: 5.5 kW
Coolant System
Maximum pressure: 10 MPa, adjustable
Maximum flow rate: 100 L/min, adjustable
Oil tank capacity: 1000 L
Filtration accuracy: 20 μm
Approximate total machine power: 30 kW
Approximate total machine weight: 6 tons
Approximate floor space: 4.5 m × 3.5 m
4. Contact Me
Email:sale@dzguanlu.com
Whatsapp/Wechat:+8613853423246
Hot Tags: zsk2202dz×500 cnc deep hole drilling machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like