Latest Products


Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com

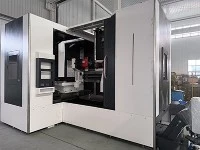
ZSK2304 Three-axis CNC Deep Hole Drilling Machine
1. Machine Overview 1.1 Drilling Method: Gun Drilling (External Chip Removal) Gun drilling principle: internal oil supply and external chip removal. The cutting fluid flows through the rotary joint at the rear end of the spindle in the drill box, the inner bore of the drill box spindle and the inner hole of the tool bar, and finally reaches the cutting edge. Carrying chips, the cutting fluid drains through the V-shaped groove on the outer surface of the tool bar into the guide holder, and then flows into the chip conveyor.
Description

1. Machine Overview
1.1 Drilling Method: Gun Drilling (External Chip Removal)
Gun drilling principle: internal oil supply and external chip removal. The cutting fluid flows through the rotary joint at the rear end of the spindle in the drill box, the inner bore of the drill box spindle and the inner hole of the tool bar, and finally reaches the cutting edge. Carrying chips, the cutting fluid drains through the V-shaped groove on the outer surface of the tool bar into the guide holder, and then flows into the chip conveyor.
1.2 Gun Drilling Range: φ3–φ40 mm
1.3 Drilling Depth: 1000 mm
1.4 CNC System
CNC System: SIEMENS-808D It is mainly used to control tool rotation, tool feed, workpiece rotation, cooling system, lubrication system and hydraulic station. Once the operator presses the start button, the machine will complete machining automatically according to the program.
1.5 X-axis
Controlled by the CNC system for transverse movement of the workpiece, travel: 1000 mm. Equipped with ball linear guides. A servo motor drives the ball screw via a servo reducer. The guideway surface is protected by a telescopic stainless steel cover.
The nut on the ball screw adopts a double-nut structure, which is lubricated at fixed time and quantity by an automatic lubrication station. Special bearings for ball screws are mounted at both ends of the screw, adopting a bearing configuration with one end fixed and the other end pre-tensioned.

1.6 Y-axis
Controlled by the CNC system for vertical movement of the tool, travel: 1000 mm. Equipped with ball linear guides. A servo motor drives the ball screw via a servo reducer. A counterweight block is used for weight balancing.
The nut on the ball screw adopts a double-nut structure, which is lubricated at fixed time and quantity by an automatic lubrication station. Special bearings for ball screws are mounted at both ends of the screw, adopting a bearing configuration with one end fixed and the other end pre-tensioned.

1.7 Z-axis
Controlled by the CNC system for longitudinal tool feed to achieve a drilling depth of 1000 mm. Equipped with ball linear guides. A servo motor drives the ball screw via a servo reducer.
The nut on the ball screw adopts a double-nut structure, which is lubricated at fixed time and quantity by an automatic lubrication station. Special bearings for ball screws are mounted at both ends of the screw, adopting a bearing configuration with one end fixed and the other end pre-tensioned.

1.8 T-slot Worktable
Dimensions: 1500 mm × 1000 mm; T-slot width: 22 mm. It can move along the X-axis bed.
1.9 Drill Box (Spindle Head)
It controls tool rotation. The servo main motor drives the spindle from the front side after speed reduction, facilitating tool change and protecting the main motor. The spindle output speed is steplessly adjustable. Main motor power: 15 kW; maximum spindle output speed: 5000 r/min.
1.10 Tool Bar Support
It is used to support the tool bar. The support sleeves mounted on the tool bar support and the support sleeve fitted at the right end of the guide holder support the tool bar to improve its rigidity.
1.11 Guide Holder
It functions for tool guiding, chip removal and tool bar support. Controlled by the pneumatic system, the guide holder automatically clamps and releases the workpiece.
1.12 Cooling System
Components: chip conveyor, circulation pump, paper tape filter, oil chiller, pump unit, liquid level sensor, flow sensor, pressure sensor, temperature sensor and oil tank. Floor-mounted oil tank, fully welded with high-quality steel plates. Various sensors are installed on the cooling system. Liquid level, oil temperature, flow rate and pressure values are displayed on gauges.
Pump unit: one set of variable frequency pump. The pump output flow is adjusted by changing the motor speed. A manual overflow valve is fitted at the pump outlet to regulate the pump output pressure.
Chip conveyor: removes chips and drains cutting fluid into the dirty oil tank. Circulation pump: delivers cutting fluid from the dirty oil tank to the filter. Paper tape filter: removes impurities from the cutting fluid coming from the dirty oil tank, with automatic paper feeding function. Oil chiller: cools the cutting fluid and starts/stops automatically according to the preset upper and lower limits of oil temperature.
1.13 Guarding
The main machine is equipped with full guarding as standard. The design fully takes into account the convenience for workpiece loading/unloading and machine operation.
1.14 Base components including bed, worktable, boxes and column are cast from high-quality cast iron and subjected to stress relief by aging treatment.
1.15 Pneumatic System
It controls the axial movement of the guide holder to clamp or release the workpiece.
2. Main Machine Parameters
Working Range
Drilling diameter range: Φ3~Φ40 mm
Maximum machining depth: 1000 mm
Machine Performance
X-axis Travel: 1000 mm
Rapid traverse speed: 4000 mm/min
Servo motor power / torque: 3.5 kW / 22 Nm
Y-axis Travel: 1000 mm
Rapid traverse speed: 3000 mm/min
Servo motor power / torque: 2 kW / 15 Nm
Z-axis Feed speed range: 5~500 mm/min
Rapid traverse speed: 3000 mm/min
Servo motor power / torque: 1.5 kW / 8 Nm
Worktable
Dimensions (X × Z): 1500 × 1000 mm
Load capacity: 6 tons
Drill Box
Maximum rotating speed: 5000 r/min
Motor power: 15 kW, servo main motor
Cooling System
Maximum pressure: 10 MPa, adjustable
Maximum flow rate: 150 L/min, adjustable
Others
Total machine power (approx.): 48 kW
Machine footprint: 5 m × 5 m
3.Other Machine
4.Contact Me:
Email:sale@dzguanlu.com
Wahtsapp:+8613853423246
Hot Tags: zsk2304 three-axis cnc deep hole drilling machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like