Latest Products


Contact Us
Add: No.21, D Zone Jingjinluji Industry Park, Xingfu Road, Dezhou City, Shandong, China
Whatsapp/Wechat: +8615165964868
SKYPE: susanleeguobin
Email: dzguanlu@dzguanlu.com
Official webiste: www.dzgljc.com
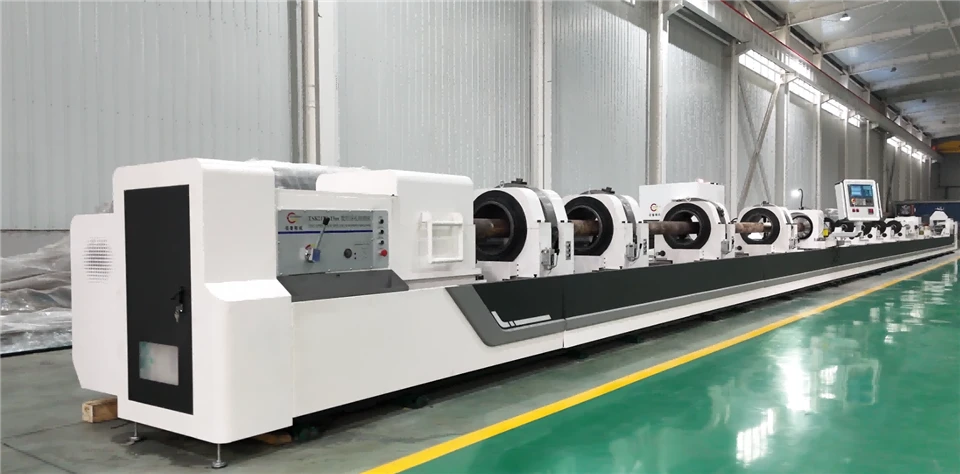
Cylinder BTA Deep Hole Drilling And Boring Machine
Solid drilling diameter range :25-80mm Boring diameter range :40-160mm Workpiece OD range :60-300mm
Description
Cylinder BTA deep hole drilling and boring machine
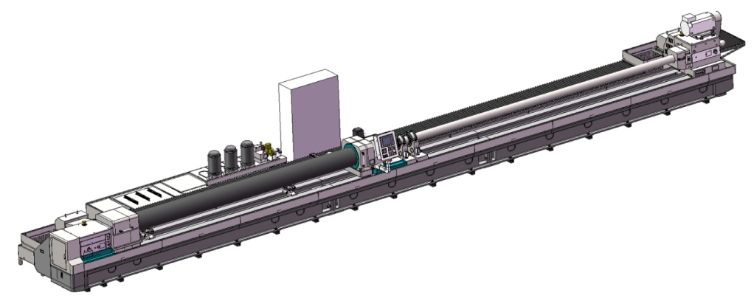
1.1 Machine processing range:
Solid drilling diameter range :25-80mm
Boring diameter range :40-160mm
Workpiece OD range :60-300mm
1.2 Machine function:drilling and push boring.
Drilling:BTA drilling method, chip is discharged backward through the drilling bar.
Boring:Push boring method, chip is dispatched forward through the bottom hole of the workpiece.
1.3 Machine main structure:
1.3.1 Machine main components:machine bed, headstock, workpiece support rest , oil pressure head, boring bar support rest, drill box, slide rail, rack and pinion,coolant system, control system, electric box, center rest.
1.3.2 Workpiece clamping method:
The manual three-jaw chuck on the headstock clamps one end of the work piece, the chuck on the oil pressure head clamps other end of the work piece.
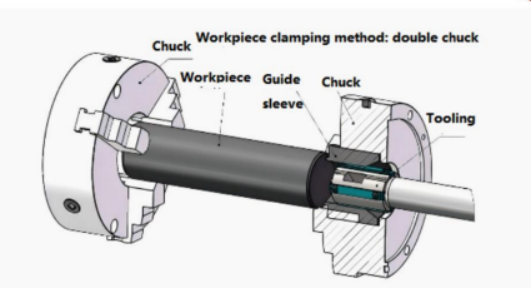
1.3.3 Machine system:DELTA PLC controller
Z-axis: the drill box is fed longitudinally, and the servo motor drives the rack and pinion mechanism through the reduction mechanism.
X axis: the oil pressure head servo jacking the workpiece, the servo motor drives the rack and pinion mechanism through the reduction mechanism.
1.3.4 The machine bed, box body, pallet and other basic parts are made of high-quality cast iron precision casting. After the casting is completed, they undergo two aging treatments to eliminate internal stress, stabilize structure and size, and improve mechanical properties.
1.3.5 Machine bed:
The bed body was cast with resin sand and normalized treatment was carried out after casting. The bed body adopts a split structure, which is assembled together by high-strength bolts and positioned by conical pins.
Adopt double rectangular sliding guide, precision grinding, high hardness of guide surface quenching.
The bed is equipped with a bevel rack for the tool feed drive. The rack is precision machined and quenched. The machine tool has large bearing capacity, rigid foot and stable transmission.
V-shaped inclined bar is arranged inside the bed body, which has large support strength and is not easy to deform. The outer wall of the bed directly supports the guide rail, the guide rail can withstand large cutting force, the rigidity of the guide rail is good, and the processing process is not easy to deform and shake, which is conducive to improving the processing quality and efficiency of the machine tool.
The oil return tank is cast around the bed body, and the oil baffle is installed on the return oil tank, and the cutting oil on the bed body automatically returns to the cooling tank.
1.3.6 Headstock:
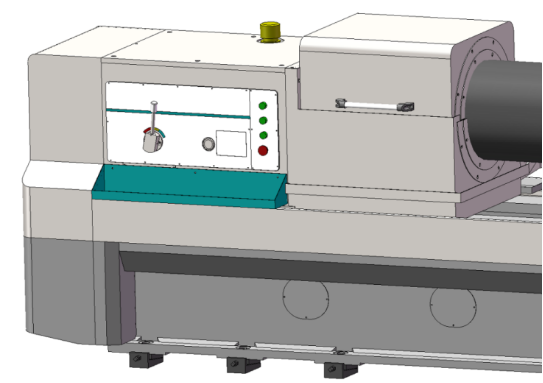
Used to drive the rotation of the workpiece, fixed on the left end of the bed body.
Manual 3 gear, stepless speed adjustment in the gear, with the servo spindle motor through the belt, gear box to drive the spindle rotation, headstock front assembly manual three-jaw chuck for clamping workpiece.
Gear precision grinding processing; The gear tooth surface is treated by high-frequency quenching, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and impact load.
The external lubricating oil box is used for circulating lubrication of gears and bearings, and low liquid level alarm device is installed in the oil tank.
A button plate is installed on the headboard box, which has the functions of spindle point, feed forward, feed backward and emergency stop.
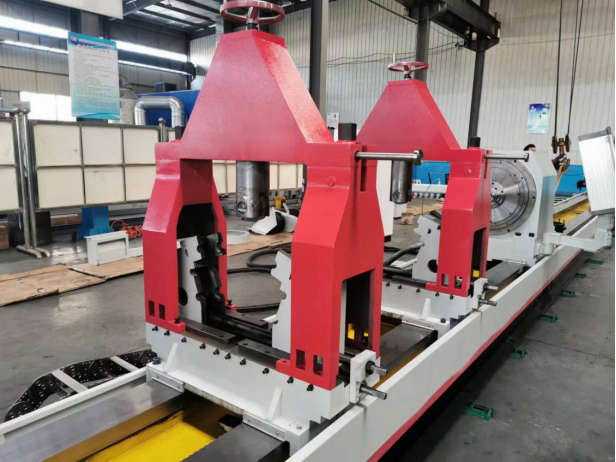
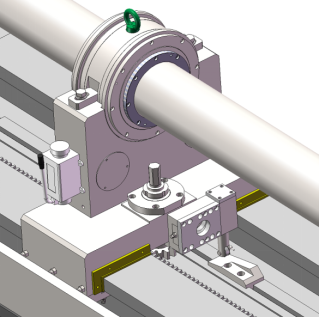
1.3.7 Center rest:The center rest is used to support the workpiece; the three-point closed center rest structure has two rollers on the bottom and one roller on the top; the two rollers on the bottom are used to adjust the lateral position through a screw.
1.3.8 Oil pressure head:
Used for tool guide, tool oil supply, tool bar support.
The servo motor is used to drive the axial movement of the workpiece to adapt to the processing of different lengths of the workpiece, and to tighten and loosen the workpiece. The servo motor can operate in torque mode or position mode.
The oil receiver rotary bearing is installed inside the oil receiver body, which has good rigidity and high rotary accuracy.
The rotary seal is installed on the outside of the right end of the oil receiver body for easy maintenance.
The right end of the oil receiver is equipped with a tool bar support sleeve for supporting the tool bar.
The left end of the oil receiver is installed with a guide sleeve and chuck.
The oil blocking device is a push-pull structure, and the oil box is installed at the lower part of the oil blocking device to make the cutting oil flow back to the oil tank.
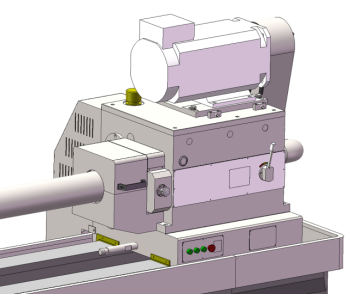
1.3.9 Drill box
Used to drive tool rotation, mounted on the feed plate.
Manual 3, stepless speed adjustment in the gear, with the servo spindle motor through the belt, belt wheel, gear system to drive the spindle rotation.
The left end of the spindle is equipped with a tool handle connecting sleeve for clamping the tool.
The right end of the spindle is equipped with a chip hopper for discharging chips.
Gear precision grinding processing; The gear tooth surface is treated by high-frequency quenching, so that the gear can obtain high strength, high hardness, high wear resistance and high fatigue limit, and can withstand relatively large alternating load and impact load.
The external lubricating oil box is used for circulating lubrication of gears and bearings, and low liquid level alarm device is installed in the oil tank.
1.3.10 Drill bar support rest:
Used to support the tool bar;
The high rigidity of the integral structure, which is equipped with support sleeve, can absorb the impact of the processing process, shake and so on.
Install the automatic hanging mechanism, the feed plate can automatically pull the tool bar support back to the initial position when the tool is withdrawn.
1.3.11 Coolant system:
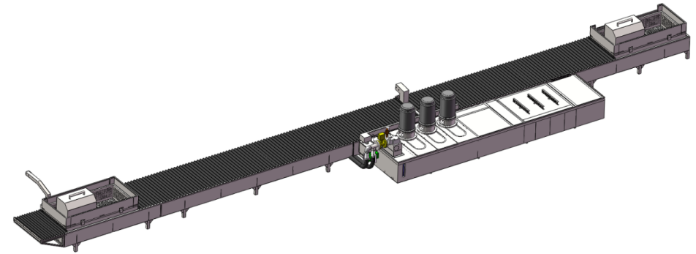
It is mainly composed of cooling pump, chip box, oil tank, etc., to provide enough cutting oil for deep hole processing.
Above ground oil tank, the oil tank adopts high quality steel plate full welding treatment.
A retractable protective cover is installed between the chip receiving boxes on the oil tank to cover the oil tank to avoid debris falling into the oil tank.
Cutting oil pressure, liquid level, oil temperature, flow, can be digitally displayed on the control station.
1.3.12 Feeding carriage:
Used to drive tool axial movement.
Automatic lubrication station is used to lubricate the sliding guide rail surface regularly and quantitatively.
The push-button plate is installed on the support plate, which has the functions of moving the main shaft of the drill pipe box, feeding forward, feeding backward and emergency stop.
1.3.13 Lubrication system:
The sliding guide rail surface of the feed plate adopts automatic lubrication station when quantitative lubrication, with low level alarm function.
Headstock bearings and gears are lubricated by an independent external oil tank with low liquid level alarm function.
The bearing and gear of drill pipe box are lubricated by independent external oil tank and have low liquid level alarm function.
The oil receiver bracket and the tool bar bracket are lubricated by manual lubrication pump.
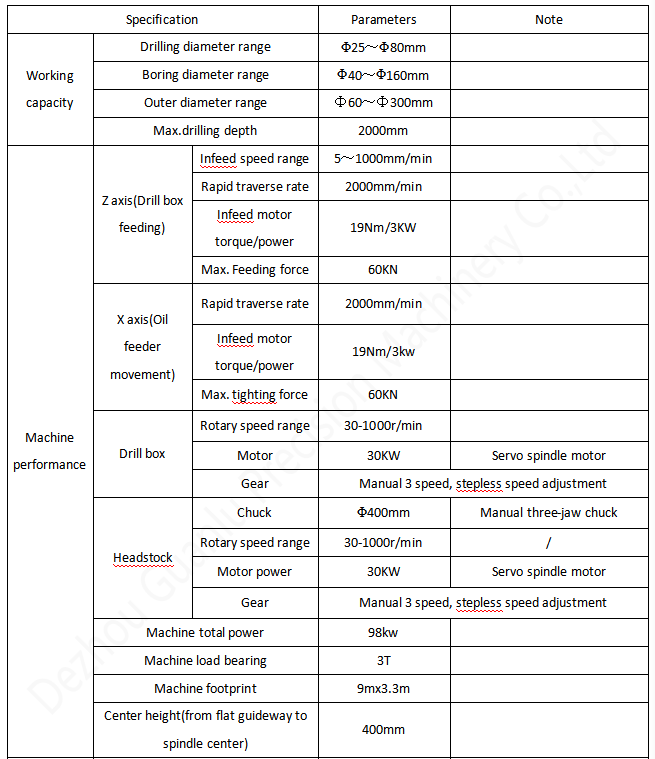
1.4 Main parameters:
More details, please feel free to contact me!
Sunny Lee: +86 15153489925; dz@dzguanlu.com
https://www.dzgljc.com/btadeepholedrillingmachine/deepholedrillingmachine.html
Hot Tags: cylinder bta deep hole drilling and boring machine, China, suppliers, manufacturers, factory, customized, price, cheap, company, cost, for sale
You Might Also Like